16 years one-stop China custom CNC machining parts factory
Hey there I’m VMT Sam!
With 25 years of CNC machining experience we are committed to helping clients overcome 10000 complex part-processing challenges all to contribute to a better life through intelligent manufacturing. Contact us now
 714 |
Published by VMT at Sep 28 2026 | Reading Time:About 8 minutes


Producing thin metal components with intricate geometries often presents a major challenge. Traditional stamping or laser cutting can introduce undesirable thermal stress, micro-burrs, or high tooling costs that compromise part performance.
To overcome these limitations, etching technology, primarily Chemical Etching (Wet Process) and Plasma Etching (Dry Process), has become the preferred solution. Unlike mechanical cutting or laser ablation, etching uses chemical or gas reaction to selectively remove material, delivering stress-free, burr-free, and high-precision metal parts or surface markings with zero thermal deformation.
In this article, you will learn about the working principles, primary types, key applications, and practical limitations of etching to help you determine if it is the right fit for your project. At the end, we will also share a real-world case study on how our factory utilized chemical etching to achieve a high-durible, and uniform micro-textured surface for medical implants.
What is etching?
Etching usually refers to photochemical etching, which refers to removing the protective film of the area to be etched after exposure and development of the plate, making the metal contact with the chemical solution during etching, and using two positive patterns to achieve the effect of dissolution and corrosion through chemical grinding from both sides.
To form the effect of concave-convex or hollow molding, chemical etching is very targeted. It refers to controlled corrosion. It is a controllable machining method for metals through chemical methods.
Different etchants have different corrosion characteristics and strengths for different metal materials. Etching is divided into dry etching and wet etching. Dry etching technology is further divided into reactive ion etching (RIE), sputter etching and vapor phase etching.
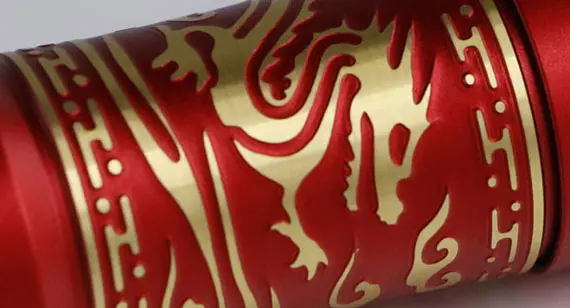
Laser Etching and Engraving Technology: They are NOT Etching
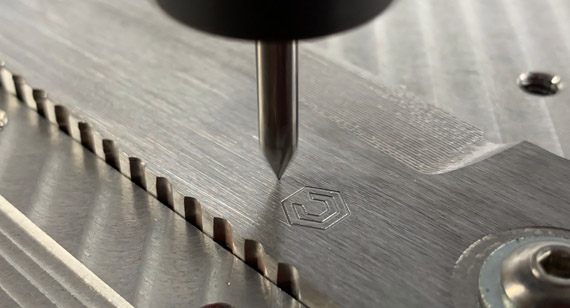
In an engineering sense, "etching" usually refers to chemical etching or plasma etching, whereas laser etching and laser engraving are actually subcategories of laser marking.
During laser etching, the extreme heat of the laser beam melts the metal surface after metal contact. After melting, the molten material expands, leaving marks on the surface of the material.
Laser etched designs are generated by graphic design software. This graphic design software supports vector files. Once the design is complete, it is saved as a vector file and transferred to a laser etcher for printing. Laser etchers use CNC routers to read out vector files. It also determines the pattern of laser movement and creates the desired design.
The purpose of anodizing aluminum is to convert the surface layer of aluminum to aluminum oxide. This material is more resistant to corrosion and wear than the pure aluminum that hides beneath it. Although aluminum oxide is practically transparent, some anodizing methods produce porous aluminum oxide layers that can be colored with special dyes. Therefore, anodized aluminum parts is more durable than regular aluminum parts and will not corrode, scratch or break. And it's available in many colors -- many advantages.
The anodizing process only affects the surface of the aluminum to a depth of 0.1-1.0mm. This makes the laser etching process, with an impact depth of only 0.25 mm, the best choice for marking anodized aluminum. In contrast, laser engraving has an impact depth of 3 mm, which means the laser exposes the less durable aluminum beneath the anodic layer, making the item more vulnerable to damage.
Laser etching and engraving technology is used in a wide variety of industries to mark postage stamps, monograms and barcodes. Their techniques are similar, but there are differences.
The main difference between laser etching and engraving processes is the depth of cut. Laser engraving penetrates the entire aluminum material, while laser etching is a shallow cut that only partially cuts through the material.
Laser etching is often used on anodized aluminum because it does not remove the anodized layer. This program can be used for serial numbers, barcodes or other drawings that need to be displayed but not deep.
Wet etching:
Wet etching is to immerse the wafer in a suitable chemical solution, or spray the chemical solution onto the wafer for quenching, and remove the atoms on the surface of the film through the chemical reaction between the solution and the object to be etched, so as to achieve the purpose of etching. Perform wet etching During etching, the reactants in the solution first diffuse through the stagnant boundary layer, and then reach the wafer surface, where chemical reactions occur to produce various products. The products of the etch chemical reaction are liquid or gas phase products, which then diffuse through the boundary layer and dissolve into the main solution. Wet etching not only etches vertically, but also etches horizontally.
Dry etching:
Dry etching is usually a type of plasma etching or chemical etching. Due to the different etching effects, the physical atoms of the ions in the plasma, the chemical reactions of the active radicals, and the surface atoms of the device (wafer), or a combination of the two, include the following:
Dry etching is an anisotropic etching with good directionality but poorer selectivity than wet etching. In plasma etching, plasma is a partially dissociated gas in which gas molecules are dissociated into electrons, ions, and other highly chemically reactive species. The biggest advantage of dry etching is "anisotropic etching". However, (radical) dry etching is less selective than wet etching. This is because the etching mechanism of dry etching is physical interaction; therefore, the impact of ions can remove not only the etching film but also the photoresist mask.
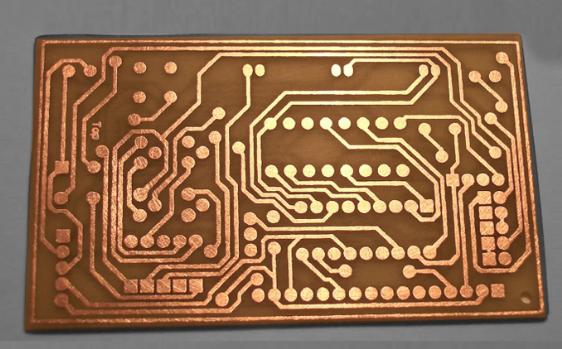
Dry etching is more often used for electronic components and semiconductorrs:
Comparison Table for Wet Etching vs. Dry Etching
Wet etching vs dry etching is importance for parts precision and related to project cost and production. It is highly recommended that you can choose Dry Plasma Etching for semiconductors, microelectronics, or microfluidic wafer chips. AND, you can choose Wet Etching for precision metal components, thin shims, EMI shielding enclosures, mesh filters, or intricate decorative patterns with zero thermal deformation or burrs.
Below is a detailed table showcasing their key differences:
| Comparison Feature |
Wet Chemical Etching |
Dry (Plasma) Etching |
| Working Mechanism |
Uses liquid chemical solutions (acids, bases, or salts) to dissolve target materials. |
Uses reactive plasma, ions, or gas phase reactions to physically or chemically remove materials. |
| Etch Directionality (Profile) |
Isotropic: Etches equally in all directions, creating an undercut/etch factor. |
Anisotropic (or Directional): Etches vertically, allowing high aspect ratio features with minimal undercut. |
| Resolution and Precision |
Micron scale (typically >=10μm), ideal for thin sheet metals, shims, and meshes. |
Sub-micron to Nanometer scale (down to < 10nm), essential for ICs, wafers, and MEMS. |
| Material Compatibility |
Stainless steel, copper, aluminum, titanium, nickel alloys, brass, and plastics. |
Silicon, Silicon Dioxide , Gallium Nitride, and thin semiconductor films. |
| Equipment and Tooling Cost |
Lower equipment cost; low tooling setup cost, making it ideal for prototyping and mass production. |
Very high equipment cost (vacuum chambers, plasma generators) and higher operating expenses. |
| Stress and Thermal Impact |
Burr-free and stress-free; does not alter the physical or mechanical properties of the metal. |
No mechanical stress, but localized ionic bombardment can introduce surface modifications. |
| Throughput and Production Speed |
High throughput (allows multi-sheet continuous spraying or batch chemical dipping). |
Moderate to low throughput (limited by vacuum processing time per batch/wafer). |
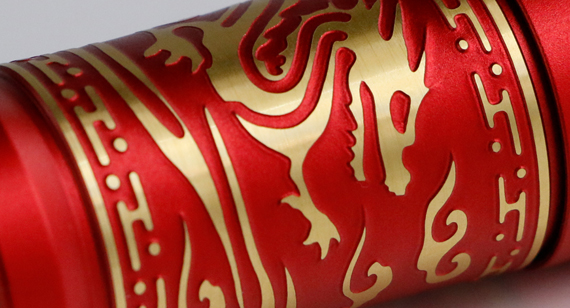
While etching is widely recognized as a surface treatment process for decorative patterns, surface texturing, and marking, it also plays a critical role in precision part manufacturing (photochemical machining).
Depending on your design requirements, etching is primarily utilized in two ways:
1. Precision Surface Treatment and Micro-Texturing
As a surface finishing process, controlled etching modifies the metal's surface properties without cutting through the material. Common applications include:
2. Full-Thru Part Manufacturing (An Alternative to Stamping)
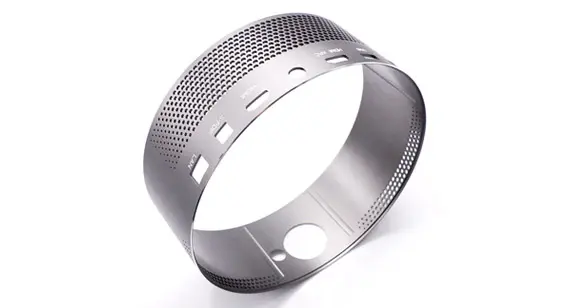
When etchants penetrate entirely through thin sheet metals, etching transforms from a surface finish into a high-precision manufacturing method. It serves as an ideal alternative to stamping or laser cutting for ultra-thin parts, producing:
Burr-free components: EMI/RFI shielding enclosures, micro-mesh filters, precision shims, and encoder disks with zero thermal stress or mechanical distortion.
For thin metal components and custom surface finishing, chemical etching provides an exceptionally versatile solution. Depending on your project requirements, its key advantages over alternative manufacturing and marking technologies include:
1. As a Part Manufacturing Process (Chemical Etching vs. Stamping and Laser Cutting)
When used for full-thru cutting of thin metal parts, chemical etching offers distinct manufacturing benefits:
2. As a Surface Treatment Process (Chemical Etching vs. Laser Etching and Laser Engraving)
When used for surface texturing, depth-controlled etching, or marking, chemical etching stands out from laser-based alternatives:
VMT’s etching process is mainly customized for incoming drawings. It can etch various materials, with a thickness ranging from 0.03MM to 2.0MM; the minimum tolerance can be controlled at 0.0075mm, and the best engineering drawings are mainly CAD engineering drawings.
2. Preparation of raw materials
Zhuolida etching process mainly involves stainless steel (201, 202, 301, 304, 316 and 400), copper, aluminum alloy, titanium alloy, among which stainless steel (201, 202, 301, 304 , 316 and 400).
3. Cleaning process
The process before stainless steel or other metal etching is cleaning treatment, the main function is to remove dirt, dust, oil stains, etc. on the surface of the material. The cleaning process is the key to ensure good adhesion of the subsequent film or screen printing ink to the metal surface. Therefore, the oil and oxide film on the metal etching surface must be thoroughly removed. Degreasing should be determined according to the oil pollution of the workpiece. It is best to carry out electric degreasing before the screen printing ink to ensure the degreasing effect. In addition to the oxide film, the best etching solution should be selected according to the metal type and film thickness to ensure the surface is clean. Must be dry before screen printing. If there is moisture.
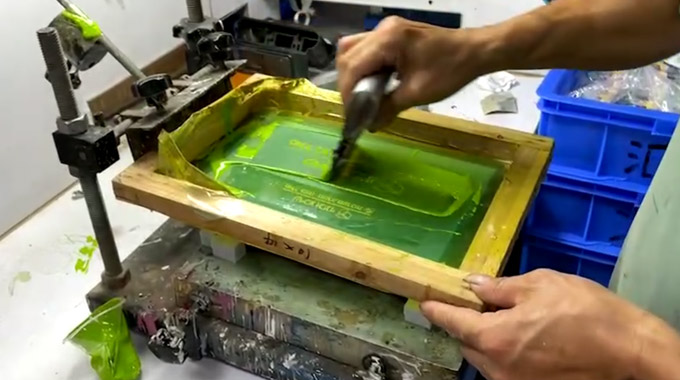
4. Paste dry film or silk screen photosensitive adhesive layer
According to the actual product material, thickness, and the precise width of the graphic, it is determined to use dry film or wet film silk screen printing. For products with different thicknesses, factors such as the etching machining time required for product graphics should be considered when applying the photosensitive layer. Thicker or thinner photoresist layers can be made with good coverage and high definition patterns produced by metal etching.
5. Exposure
Exposure, transfer imaging through photomask UV exposure.
This process is an important process of metal etching, and the exposure energy will be considered according to the thickness and precision of the product material. This is also a reflection of the technical capabilities of etching machining enterprises. The exposure process determines whether etching can ensure better dimensional control accuracy and other requirements.
6. Development
After exposing the photosensitive adhesive layer on the surface of the metal etching plate, the pattern adhesive layer is cured after exposure. Afterwards, the unwanted parts of the pattern, that is, the parts to be etched, are exposed. The development process also determines whether the final dimensions of the product will meet the requirements. This process will completely remove the unwanted photoresist layer from the product.
7. Drying
After the film or roller screen printing ink is finished, the photoresist layer needs to be thoroughly dried in preparation for the exposure process. At the same time, it is necessary to ensure that the surface is clean and free of adhesions and impurities.
8. Etching
After the product prefabrication process is completed, the metal is corroded by the etching solution. This process determines whether the final product is qualified or not. This process involves parameters such as the concentration, temperature, pressure, and speed of the etching solution. The quality of the product needs to be determined by these parameters.
9. Remove
The surface of the etched product is still covered with a layer of photosensitive adhesive, and the photosensitive adhesive layer on the surface of the etched product needs to be removed. Since the photosensitive adhesive layer is an acidic substance, the acid-base neutralization method is mostly used for puffing. After overflow cleaning and ultrasonic cleaning, the photosensitive adhesive layer on the surface is removed to prevent photosensitive adhesive residue.
10. Detection
After the film is taken, the follow-up is testing, packaging, and the final product confirms whether it meets its specifications. Standardized packaging, put each product into the corresponding packing box, and register the corresponding details.
1. Reduce side corrosion and protruding edges, and improve metal etching machining coefficient: Generally, the longer the printed board is in the metal etching solution, the more serious the side etching will be. Undercut seriously affects the accuracy of printed lines, and severe undercuts will not be able to make thin lines.
The etch factor increases as undercuts and edges decrease. A high etch factor indicates the ability to maintain thin lines and bring etched lines close to the original image size. Whether the plating resist is tin-lead, tin, tin-nickel, nickel, etc., excessively protruding edges can cause shorts in the wires. Since the protruding edge breaks off easily, a bridge is formed between the two points of the wire.
2. Improve the consistency of etching machining rate between plates: in continuous plate etching, the more consistent the metal etching process rate, the more uniform etched plates can be obtained. In order to always maintain the best etching state during the pre-etching process, it is necessary to choose an etching solution that is easy to regenerate and compensate, and the etching rate is easy to control.
Choose techniques and equipment that provide constant operating conditions and enable automatic control of various solution parameters. It can be realized by controlling the amount of dissolved copper, PH value, solution concentration, temperature, uniformity of solution flow, etc.
3. Improve the uniformity of metal etching machining speed on the entire board surface: the etching uniformity of the upper and lower sides of the board and each part of the board surface is determined by the uniformity of the flow rate of the metal etching solution on the board surface.
During the etching process, the etching rates of the upper and lower plates are often inconsistent. The etch rate of the lower side is higher than that of the upper side. Due to the accumulation of solution on the surface of the upper plate, the etching reaction is weakened. The uneven etching of the upper and lower plates can be solved by adjusting the injection pressure of the upper and lower nozzles. With a spray system, oscillating nozzles, the uniformity of the entire surface of the board can be further improved by making the spray pressure different in the center and edge of the board.
Exposure and development problems
Etching machining is highly targeted, and metals are usually processed by chemical etching, so etching machining can also be called chemical etching machining. Common problems in chemical etching machining are as follows:
1. The rough etched surface has pitting and grooves after being etched. The main reason is that the concentration of acidic etching solution in the etching solution is too high, pickling after etching, pickling is not clean, the solution is to adjust the concentration of the components of the etching solution to meet the specified range of the process.
2. There are pits on the etched parts. This is because the concentration of the etching solution NaOH and AI3 is too high, just dilute the etching solution and reduce the concentration.
3. The edge line of the contour is very blurred. In this case, the surface of the raw material of the etched part has not been cleaned, and there are oxide films, chemical pollution, ink, etc. The solution is to establish an effective and reasonable cleaning of the raw material before entering the exposure and development. Cleaning process.
Metal etching provides a stress-free, burr-free manufacturing solution for ultra-thin and intricate metal parts across diverse high-tech industries.
Whether utilized for stress-free precision component manufacturing or engineered micro-surface modification, chemical etching provides an unmatched balance of precision, speed, and cost efficiency. By avoiding the mechanical forces of traditional metal stamping and the heat-affected zones of laser cutting, etching ensures that your thin metal parts retain their native mechanical properties with zero burrs and zero thermal distortion. From aerospace shims and electronic micro-meshes to surface-textured medical implants, mastering etching techniques also allows your teams to overcome tight-tolerance manufacturing bottlenecks while maintaining strict quality standards and ideal surface effects. Looking for the chemical etching services to lower your tooling costs, remove deburring, and accelerate your time-to-market? Welcome to contact us and upload your drawings for free revew of part geometries, material compatibility, and tolerance requirements with DFM analysis and quote, and the respone will be in one business day. [2D Drawings (PDF files), 3D Drawings (IGS/STP/STEP files)].
Send your 2D drawings, 3D CAD models, material, thickness, tolerance, feature size, surface-finish requirements, prototype quantity and production quantity. VMT will review etching feasibility, DFM, process selection, inspection and quotation requirements.
All information and uploaded files are secure and confidential.
1 Tell us what you need
2 Get solution & quote
3 Approve production
Email: inquiry@vimetal.com.cn
VMT CNC Machinin Factory Case Study
Optimizing Medical Implant Surface Details via Chemical Etching
A leading medical device manufacturer approached our factory to address specific surface finish consistency requirements for their titanium orthopaedic implants. The client's previous supplier used traditional CNC machining and sandblasting processes, which left subtle tool direction marks and minor edge micro-burrs along complex contours. The resulting uneven surface light reflection and localized finish variations led to unnecessary cosmetic rejections and made it difficult to achieve a completely uniform matte appearance required for medical-grade components.
To achieve the exact surface uniformity requested, our engineering team utilized a specialized wet chemical etching process suited for medical-grade titanium alloy for the client. Operating through controlled chemical spray atomization, the process selectively dissolved surface material at the micron level. This non-contact technique cleanly removed minor machining lines and micro-burrs without introducing mechanical stress or altering the core component dimensions.
The chemical etching process produced a highly consistent, non-reflective micro-textured surface profile (Ra 1.6 um +/- 0.2 um) across all complex geometric contours. This controlled micro-roughness significantly increased the effective surface area, providing ideal physical anchoring sites for superior mechanical interlocking. Furthermore, the process fully met the strict cleanliness and residue limits outlined in ISO 19227 (Cleanliness of orthopedic implants) and ASTM F88, reducing total organic carbon (TOC) levels to below 10 ug/cm2 and completely eliminating residual grit or metallic particles.
By integrating controlled wet chemical etching into the manufacturing workflow, our engineering team helped the client reduce post-processing rework rates from 12% down to 0.5%, achieve a 99.2% first-pass yield, and maintain batch-to-batch dimensional consistency within +/-0.01 mm. This precise surface treatment allowed the implants to seamlessly pass quality inspections and proceed directly to cleanroom packaging.
1. What is the maximum thickness for chemical etching?
Chemical etching is typically suitable for sheet metals up to 1.5 mm to 2.0 mm thick, as etchant undercut increases with thicker material.
2. Is chemical etching cheaper than stamping for low volumes?
Yes, chemical etching uses low-cost digital photo-tooling rather than expensive steel dies, making it significantly more economical for low-to-medium volumes and rapid prototyping.
3. Does chemical etching cause stress or burrs on metal parts?
No, because chemical etching removes material via chemical dissolution rather than mechanical force or intense heat, it produces completely stress-free and burr-free components.
4. What metal alloys can be chemically etched?
Chemical etching works exceptionally well on a wide range of metals, including stainless steel, copper alloys, brass, aluminum, nickel, titanium, and nitinol.
5. How tight are the tolerances achievable with chemical etching?
For thin-metal part manufacturing and fine feature etching (such as micro-holes or complex mesh), it is usually achievable the tolerances range from ±0.01 to 0.025mm. And when it is used as as a surface treatment on pre-machined CNC parts, controlled chemical etching selectively removes material at the micron level without altering or compromising the original mechanical tolerances or introducing stress.
6. What is the typical lead time for chemically etched parts compared to stamping?
Since photo-tooling can be prepared digitally within hours, prototype turnaround times for chemical etching are usually 2 to 5 days, compared to weeks or months required for stamping dies.
The technical information and manufacturing advice shared on the VMT website are for general guidance only. While we strive for accuracy, VMT does not guarantee that the processes, tolerances, or material properties mentioned are applicable to every specific project. Any reliance you place on such information is strictly at your own risk. It is the buyer's responsibility to provide definitive engineering specifications for any production orders. Final specifications and service terms shall be subject to the formal contract or quotation confirmed by both parties.


 +86 15099911516



 Read more