16 years one-stop China custom CNC machining parts factory
Hey there I’m VMT Sam!
With 25 years of CNC machining experience we are committed to helping clients overcome 10000 complex part-processing challenges all to contribute to a better life through intelligent manufacturing. Contact us now
 649 |
Published by VMT at Oct 08 2026 | Reading Time:About 6 minutes


As a corrosion-resistant and cost-effective material, stainless steel is widely used in CNC machined parts such as telecommunications enclosures, architectural decorations, industrial equipment components, automotive suspensions, and wheel rims. Powder coating these stainless steel CNC machined parts is the ideal surface treatment solution to achieve your required custom colors, electrical insulation, anti-fingerprint properties, weld discoloration coverage, as well as enhanced wear and corrosion resistance in harsh industrial or acidic/alkaline environments.
However, Have you learned how powder coating impacts project cost, lead time, part assembly, and surface pre-treatment requirements? Furthermore, comparing stainless steel powder coating with other surface treatments will help you evaluate whether powder coating is the best fit for your product as well.
This article will provide a comprehensive guide and practical insights on powder coating stainless steel. At the end, we will also share a case study from our factory: outdoor high-end equipment stainless steel components where we advised the client to choose powder coating based on the application scenario, and successfully delivered one-stop manufacturing including CNC machining, sandblasting, custom color matching, and powder coating.
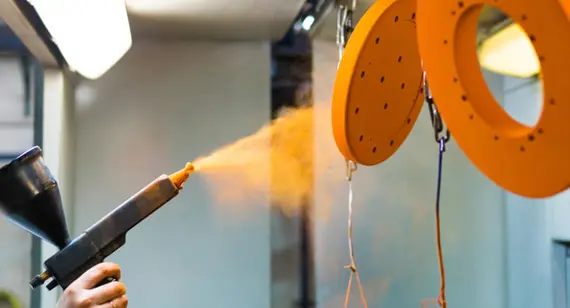
Although stainless steel inherently offers good corrosion resistance and a sleek silver-grey metallic appearance, opting for powder coating takes your parts a step further with superior protection and endless color customization. Beyond aesthetics, industrial advantages like concealing surface imperfections, enhanced wear resistance, eco-friendliness, cost efficiency, and ease of maintenance make powder coating a smart choice for stainless steel CNC parts.
The thermosetting polymer layer creates a tough protective shield that resists chipping, scratching, and daily physical wear far better than liquid paint.
It offers unlimited design flexibility, allowing you to choose from custom RAL colors, diverse textures, and varying gloss levels (from high-gloss to matte).
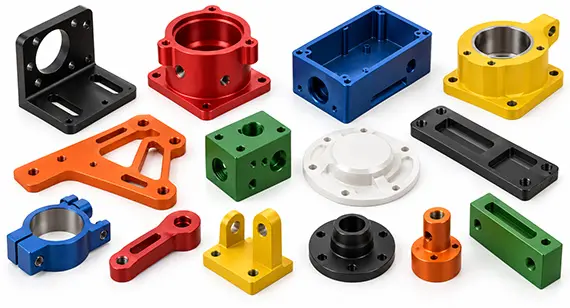
The process releases zero Volatile Organic Compounds (VOCs), and oversprayed powder can be collected and reused, significantly reducing environmental waste.
It provides an extra barrier against severe saltwater, high humidity, and aggressive chemical exposure, making it ideal for marine or chemical processing applications.
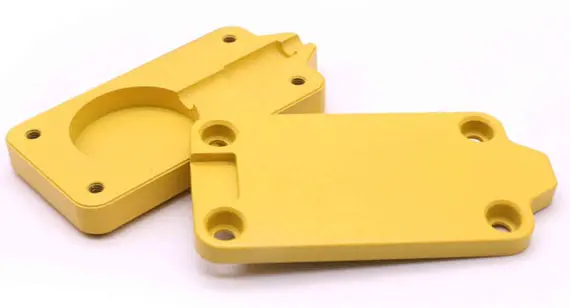
The thick, uniform coating effectively covers up visible weld seams, heat discoloration, and subtle machining marks for a flawless final appearance.
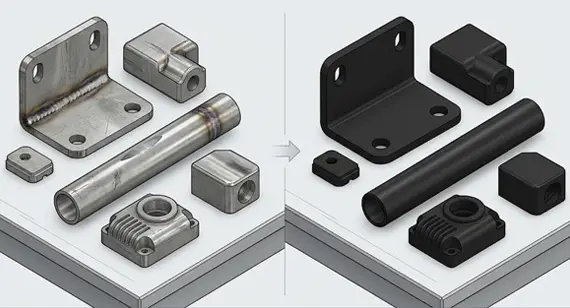
Powder coating is highly cost-effective, especially for high-volume production runs, as it significantly reduces the need for rework and touch-ups compared to traditional painting methods.
The smooth, non-porous powder-coated surface repels dirt and grease, allowing quick and simple cleaning with basic soap and water.
Once the curing oven cools down, parts are immediately ready for handling and assembly without waiting days for paint to dry.
The powder coating process for stainless steel parts involves multiple rigorous steps. An experienced CNC machining factory focuses on process control and technical details to ensure a durable, high-quality finish with maximum adhesion. Below is our typical SS powder coating workflow integrated smoothly into our one-stop CNC machining and surface finishing production lines:
1. Surface Cleaning and Pre-Treatment (Crucial Step)
Beyond removing surface oils, dirt, and greases, stainless steel naturally forms a passive chromium oxide layer that prevents raw powder from adhering properly. To tackle this, mechanical pre-treatments like abrasive sandblasting or grinding are essential to etch the surface, create an optimal micro-roughness profile, and guarantee long-term mechanical bonding.
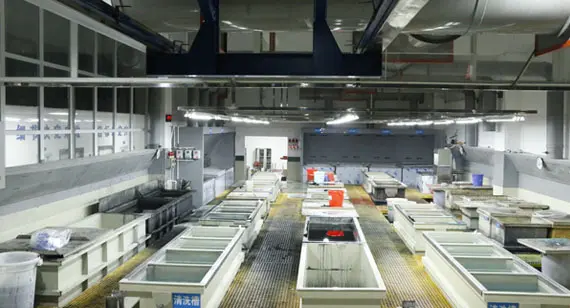
2. Stainless Steel Powder Coating Primer Application (Optional)
For parts exposed to extreme outdoor or corrosive environments, an epoxy-based or silane-based primer is applied prior to the main coat. This step significantly boosts interlayer adhesion and acts as a secondary protective shield against moisture undercut.
3. Powder Spraying in a Dedicated Spray Booth
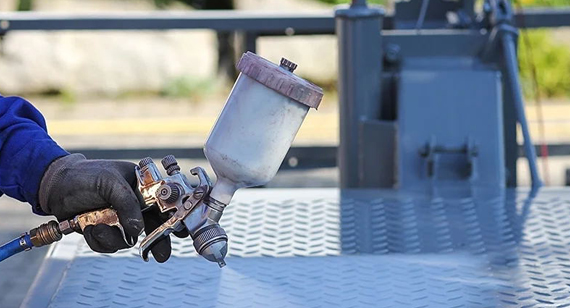
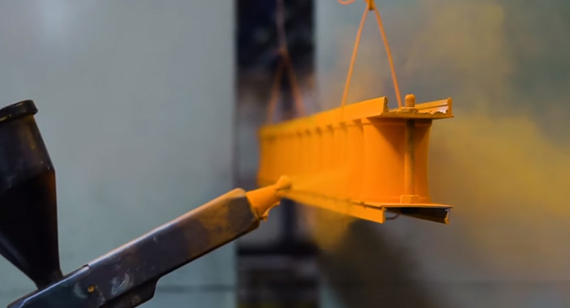
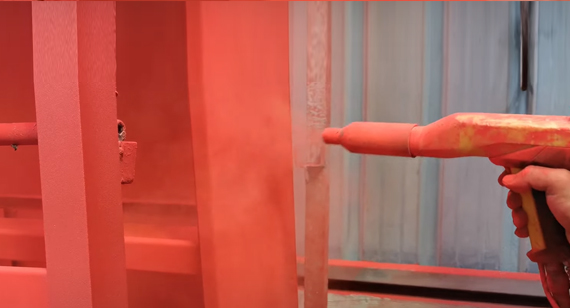
In a clean, climate-controlled spray booth, electrostatic spray guns charge the dry powder particles. These particles are evenly attracted to the grounded stainless steel part, forming a uniform, seamless coating even over complex CNC geometry.
4. Thermal Curing
The coated parts are transferred into a high-temperature curing oven (typically heated to 370°F -400°F/ 180°C-200°C. The powder melts, flows together, and cross-links chemically to form a tough, solid polymer matrix.
5. Controlled Cooling
After curing, parts are gradually cooled down in a clean environment to relieve thermal stress, preventing coating micro-cracks or premature delamination.
Every batch undergoes rigorous quality control, including cross-hatch adhesion testing, coating thickness measurement (using a digital film thickness gauge), color matching validation, and visual surface defect checks.
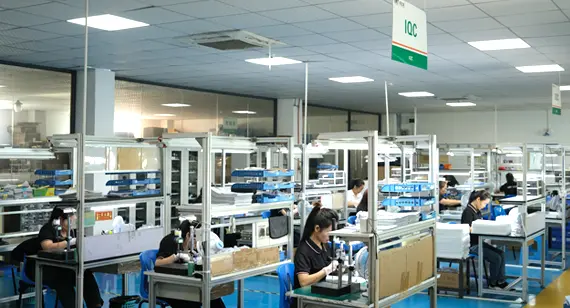
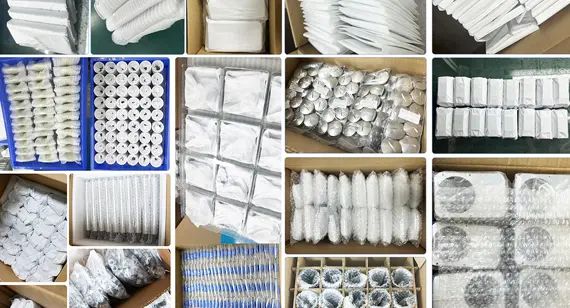
Once cleared by QC, parts are individually wrapped with protective film and custom foam packaging to prevent scratches or impact damage during international transport, ensuring they arrive at your place with well-protected quality.
Typically, a standard powder coating adds a thickness layer of 2.0 to 4.0 mils (50 to 100 microns) to the part's surface. On tight-tolerance CNC machined components, this extra layer can significantly impact critical fits, such as bearing seats, threaded holes, and precision mating surfaces. An experienced factory will account for coating thickness during the CAD/CAM programming stage by pre-calculating tolerance allowances or applying specialized silicone masking/plugs to key functional areas before spraying.
However, you may keep in mind that powder coating cannot achieve 100% absolute uniformity across complex geometries. Factors like part edges, and powder flow during oven curing cause subtle film thickness variations. To avoid assembly issues, you need to mark critical features, threaded holes, and datum surfaces on the drawings so the factory can properly mask or compensate for them.
When adding powder coating to already machined stainless steel parts, the additional cost and lead time depend heavily on batch size, pre-treatment intensity, and color selection. For a standard order of 1,000 medium-sized, simply-structured stainless steel parts in a standard RAL matte/matte-black finish, powder coating typically adds about $1.50 to $3.50 per piece (including sandblasting pre-treatment) and adds roughly 3 to 5 business days to your total production schedule.
For prototyping or small batches, setup fees and manual handling make up a higher percentage of the unit price. However, for medium-to-large production runs (1,000+ pcs), high-efficiency automated spraying lines keep per-part costs extremely low. Choosing common stock colors like matte black or traffic white or other color that the factory has can ensure the fastest turnaround without incurring custom powder blending fees.
The lifespan of powder-coated stainless steel parts varies based on the operating environment and surface preparation quality:
With minimal exposure to UV rays, harsh moisture, or chemicals, the powder coating remains intact virtually very long without peeling or fading.
UV-resistant polyester powders withstand seasonal weather, sunlight, and rain with negligible color fading.
In salt-spray, high-humidity, or acidic or alkaline environments, longevity relies heavily on mechanical sandblasting and epoxy pre-primer coats. Under proper pre-treatment, parts can generally achieve over 1,000 hours of salt spray resistance.
Standard powder coatings are electrical insulators. The cured polymer coating (such as epoxy, polyester, or polyurethane) creates a non-conductive dielectric barrier over the conductive stainless steel substrate, offering excelente insulation strength (typically ranging from 300 to 800 V/mil). This makes powder-coated enclosures and brackets ideal for electrical housing and battery components where accidental grounding must be prevented.
But for SS part that requires grounding, EMI/RFI shielding, or static dissipation (ESD protection), standard powder coating will block electrical conductivity. In such cases, you can ask the factory to mask off specific grounding points/studs, opt for specialized conductive powder coatings, or consider alternative surface treatments like passivation, electropolishing, or conductive chemical conversion coatings.
You have virtually unlimited color and aesthetic choices. Factories typically work with international standard color systems, primarily the RAL Color Chart (e.g., RAL 9005 Black, RAL 9016 White, RAL 7016 Anthracite Grey) and Pantone (PMS) matching systems.
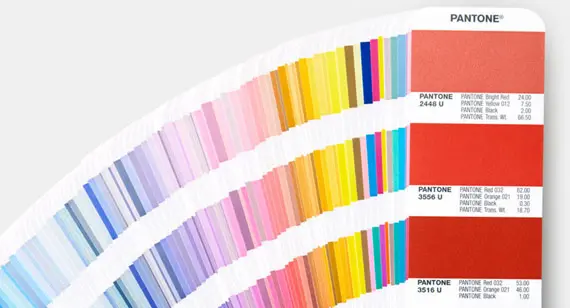
In addition to color, you can customize the finish texture and gloss level:
To achieve the most economical powder coating solution without compromising performance, consider the following tips:
While powder coating offers exceptional durability, custom color flexibility, and heavy-duty protection, stainless steel can also be finished with several other popular methods. Below is a comparison of powder coating against passivation, electropolishing, and PVD coating to help you make the right decision:
| Surface Treatment | Color and Aesthetics | Corrosion Resistance | Electrical Conductivity | Relative Cost | Examples |
| Powder Coating | Unlimited (RAL colors, custom textures, matte/gloss) | High (With proper sandblasting pre-treatment) | Non-conductive (Insulator) | Moderate | Outdoor enclosures, automotive brackets, industrial equipment, branded hardware |
| Passivation | Natural raw steel (No color change) | High (Removes free iron and restores layer) | Conductive | Low | Medical components, food-grade parts, cleanroom equipment |
| Electropolishing | Bright metallic / Mirror-like finish | Very High (Ultra-smooth surface prevents contaminant buildup) | Conductive | Moderate to High | Semiconductor equipment, pharmaceutical fittings, sanitary valves |
| PVD Coating (Physical Vapor Deposition) | Premium metallic shades (Gold, Rose Gold, Black, Titanium) | High (Extremely hard thin film) | Conductive | High | Luxury hardware, architectural trim, high-end consumer goods |
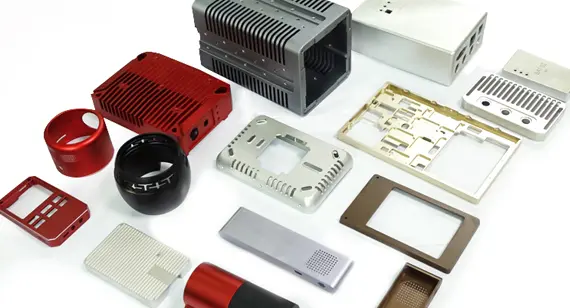
Powder-coated stainless steel and steel parts find applications in various industries and settings due to their durability, corrosion resistance, and customizable aesthetics. Here are some common applications of these powder-coated parts:
Architectural and Building Construction:
Furniture and Decorative Items:
Appliances and Electronics:
Recreational and Sports Equipment:
Marine and Offshore Applications:
Medical and Healthcare Devices:
Agriculture and Farming:
Retail Displays and Fixtures:
Aviation and Aerospace:
Oil and Gas Industry:
Electrical and Electronics Enclosures:
Food Processing and Packaging:
These are just some examples of the diverse applications of powder-coated stainless steel and steel parts. The versatility and protective qualities of powder coating make it a popular choice for enhancing both the functionality and aesthetics of various products and structures across multiple industries.
One-Stop Manufacturing and Powder Coating 316L Stainless Steel Brackets for Outdoor Telecom Enclosures
A European manufacturer of outdoor telecommunications equipment required 500 custom 316L stainless steel mounting brackets. Installed on coastal telecom towers, these structural components hold external sensor modules and housing enclosures. While 316L stainless steel provides good bulk corrosion resistance, prolonged exposure to high-salinity coastal air can lead to localized pitting corrosion along CNC machining marks. Additionally, the client required a specific matte black finish to align with their corporate equipment color standards.
Solutions
To meet the client's visual branding requirements and provide secondary barrier protection, our technical team specified an outdoor-grade thermosetting TGIC-polyester powder coat in RAL 9005 (Jet Black) with a 15% (±5%) matte finish. Polyester powder was chosen over epoxy due to its superior UV resistance against long-term solar exposure, preventing chalking and color fading in field operations.
All production steps were performed in-house within our integrated CNC machining and surface finishing line under a unified quality control system:
Results
The completed production batch underwent quality verification prior to packaging:
This article systematically introduces the advantages of stainless steel powder coating, critical surface pre-treatment (sandblasting to break the passive chromium oxide layer), the complete process workflow, and a comparison with alternative surface treatments such as passivation, electropolishing, and PVD coating. It also provides practical engineering recommendations regarding tolerance control, color selection, and cost/lead time optimization. While stainless steel inherently offers good corrosion resistance, powder coating delivers a dual upgrade in protection and aesthetics for harsh environments or specific color requirements. You can flexibly choose the most suitable surface finishing solution based on your product's actual application scenario, assembly tolerances, and budget.
For tailored advice on whether powder coating's corrosion resistance, wear resistance, cost, and lead time suit your application, or to consult on alternative stainless steel machining and surface finishing solutions, our engineering team is always here to assist with expert guidance and a free project evaluation. [Upload: 2D Drawings (PDF files), 3D Drawings (IGS/STP/STEP files)].
Send your 2D drawings, 3D CAD models, stainless steel grade, critical tolerances, coating color and texture, masking requirements, prototype quantity and production quantity. VMT will review machining, surface preparation, powder coating, DFM, inspection and quotation requirements.
All information and uploaded files are secure and confidential.
1 Tell us what you need
2 Get solution & quote
3 Approve production
Email: inquiry@vimetal.com.cn
Q1: What are the main limitations of powder coating on stainless steel?
The main limitations include minimum film thickness constraints (difficult to apply thinner than 40 microns), loss of raw metallic aesthetic, and line-of-sight or Faraday cage restrictions where powder may not easily penetrate extremely deep, narrow internal channels or blind holes.
Q2: Should I choose powder coating or liquid painting for stainless steel parts?
Powder coating is superior for high-volume production, impact resistance, and eco-friendliness (zero VOCs). Liquid painting is usually chosen only when heat-curing (180°C to 200°C) would damage sensitive internal assemblies, or when ultra-thin coating thickness (under 30 microns) is strictly required.
Q3: Can powder-coated stainless steel parts be welded or bent after coating?
Post-coating welding or bending is not recommended. Thermal heat from welding will burn and ruin the surrounding powder film, while tight-radius bending can cause the cured thermosetting polymer layer to crack. All CNC machining, bending, and welding should be completed prior to powder coating.
Q4: How does powder coating compare to PVD coating for decorative stainless steel?
Powder coating provides a thicker, cost-effective layer with solid RAL colors and matte/textured finishes for heavy protection. PVD (Physical Vapor Deposition) creates an ultra-thin, extremely hard metallic film (such as Rose Gold or Titanium Black) that preserves the natural brushed/polished metal texture at a significantly higher cost.
Q5: Can damaged powder coating on stainless steel be repaired in the field?
Yes, minor chips or scratches can be touched up using color-matched air-dry acrylic or polyurethane liquid touch-up paint. For severe surface damage, the entire part must be mechanically sandblasted or chemically stripped before re-applying a full powder coat.
Q6: Does powder coating affect tight machining tolerances or threaded holes?
Yes. Standard powder coating adds 50 to 100 microns (2.0 to 4.0 mils) of film thickness per side. For precision CNC machined parts, critical mounting features and threaded holes (e.g., M3 to M20) must be pre-adjusted in machining or protected using high-temperature silicone masking plugs prior to spraying.
The technical information and manufacturing advice shared on the VMT website are for general guidance only. While we strive for accuracy, VMT does not guarantee that the processes, tolerances, or material properties mentioned are applicable to every specific project. Any reliance you place on such information is strictly at your own risk. It is the buyer's responsibility to provide definitive engineering specifications for any production orders. Final specifications and service terms shall be subject to the formal contract or quotation confirmed by both parties.


 +86 15099911516



 Read more