Should the Drawing Dimension Apply Before or After Zinc Plating?
For any feature that controls assembly, the drawing should make clear whether the tolerance is required on the bare machined part or on the finished plated part. If the component must assemble after zinc plating, the functional acceptance dimension should normally be defined for the post-plating condition.
Example: Ø10.000 ±0.010 mm finished shaft
If the specified zinc build were approximately 8 µm per surface, the geometric diameter increase would be about 0.016 mm. Machining the bare shaft to Ø10.000 mm and then plating it would therefore risk pushing the finished shaft above the required size.
That does not mean the correct bare-machining target is automatically Ø9.984 mm. The actual pre-plating target must account for the specified minimum or controlled coating range, plating distribution, process capability and the drawing tolerance. VMT works backward from the required post-plating dimension during DFM instead of treating the pre-plating size as the final acceptance value.
How Should Zinc-Plated Bores and Precision Fits Be Designed?
A bore receives coating on its internal surface, so the usable diameter becomes smaller. For example, a nominal 8 µm build on each side gives an approximate 0.016 mm reduction in bore diameter. That may be insignificant for a loose clearance hole but critical for a bearing seat, locating bore, precision sleeve, pin fit or press fit.
For fit-critical bores, the drawing should identify one of two strategies: final size after plating, allowing the manufacturing team to establish a suitable pre-plating target; or mask / no plate when the fit cannot tolerate coating buildup. The choice depends on the permitted fit range, coating requirement and geometry.
A simple note such as “ZINC PLATED” is not enough for a precision bearing bore. Mark the critical bore, define its final acceptable size, and state whether plating is permitted on that surface.
What Should Be Done With Threads Before Zinc Plating?
Threads should not be treated as a simple smooth diameter because coating on the flanks changes the effective thread geometry and can tighten the fit. The drawing should define the required final thread designation and whether acceptance is required after plating.
For critical functional threads, VMT reviews whether the feature should receive controlled allowance, masking or another agreed process route, then checks the finished thread with the appropriate inspection method. Where GO / NO-GO gauges are specified, acceptance should reflect the finished plated condition rather than only the bare machined thread.
This is especially important for internal threads, fine pitches and assemblies where both mating components have protective finishes.
When Should a Surface Be Masked Instead of Compensated?
Not every critical feature should be controlled by machining undersize or oversize before plating. Masking is often the safer route when the available dimensional tolerance is comparable to the coating buildup or when a functional surface must retain direct base-metal contact.
Typical no-plate or masking candidates include bearing seats, precision dowel holes, electrical contact or grounding surfaces, sealing faces, tight press fits and precision locating datums. These areas should be marked directly on the drawing rather than left for the plater to decide.
How Should Zinc Coating Thickness Be Selected?
For electrodeposited zinc on iron and steel, ASTM B633 defines four standard minimum thickness classes. The correct class is selected according to the specified service condition and customer requirement; thicker is not automatically better for a precision component because dimensional buildup also increases.
| ASTM B633 Classification |
Minimum Zinc Thickness |
Service Condition |
| Fe/Zn 5 |
5 µm |
SC 1 — Mild |
| Fe/Zn 8 |
8 µm |
SC 2 — Moderate |
| Fe/Zn 12 |
12 µm |
SC 3 — Severe |
| Fe/Zn 25 |
25 µm |
SC 4 — Very severe |
A thicker coating can provide a higher corrosion-protection requirement when the specification calls for it, but it also increases external diameters, reduces internal diameters and can affect threads and tight fits. The finish type, passivation, appearance and corrosion-test requirement must therefore be reviewed together with the dimensional tolerance.
What About Hardened or High-Strength Steel?
High-strength steel requires additional review because electroplating processes can introduce hydrogen-embrittlement risk. Do not submit only “alloy steel” on the RFQ. Provide the exact grade, heat-treatment condition, hardness or tensile-strength requirement and the plating specification so the pretreatment and post-treatment requirements can be evaluated before production.
ASTM B633 also contains specific hydrogen-embrittlement provisions and states that very high-strength steels above the standard's stated limit should not simply be zinc electroplated under the ordinary specification. VMT therefore confirms the material condition before accepting the finishing route.
What Should Be Included on the Drawing and RFQ?
A clear RFQ reduces the risk that the CNC supplier, plating supplier and customer use different definitions of an acceptable finished part.
| Drawing / RFQ Requirement |
What Should Be Defined |
| Base Material |
Exact steel or iron grade. |
| Heat Treatment |
Condition, hardness or strength requirement when applicable. |
| Zinc Specification |
ASTM B633 or the customer / industry specification required by the project. |
| Coating Thickness |
Required class or thickness range where specified. |
| Passivation / Appearance |
Clear, blue or other specified finish condition. |
| Critical Dimensions |
Identify which dimensions must be accepted after plating. |
| Threads |
Final thread designation and inspection condition. |
| No-Plate Areas |
Mark masking boundaries directly on the drawing. |
| Cosmetic Surfaces |
Identify visible or appearance-critical surfaces. |
| Corrosion Test |
Specify the test only when required by the drawing or purchasing specification. |
| Inspection |
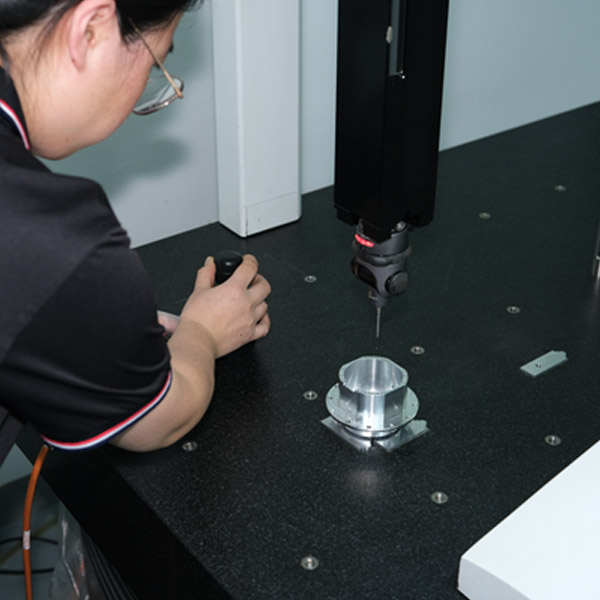
CMM, dimensional gauges, thread gauges, coating thickness or other required records. |
Before Sending Your RFQ
Send VMT your drawing, exact material grade, batch or annual quantity, zinc-plating specification and the dimensions that must be accepted after plating. If the drawing does not yet define coating allowance, masking or finished-condition tolerances, our engineers can review these items during DFM before quotation.
 +86 15099911516
 inquiry@vimetal.com.cn




 Related suggestion