16 years one-stop China custom CNC machining parts factory
Hey there I’m VMT Sam!
With 25 years of CNC machining experience we are committed to helping clients overcome 10000 complex part-processing challenges all to contribute to a better life through intelligent manufacturing. Contact us now
 357 |
Published by VMT at Sep 30 2026 | Reading Time:About 6 minutes


CNC machined brass parts possess various distinct properties, such as superior corrosion resistance, excellent machinability, and high toughness, which are primarily determined by the characteristics of different brass grades. In practical applications, considering the properties of brass types and grades is indeed essential, but it is not the only factor.
The last thing you want is to spend time and money only to run into common pitfalls: parts tarnishing shortly after machining, thin-walled features warping or cracking after processing, or plumbing components exported to Europe and America being rejected due to excessive lead content. Additionally, overlapping brass designation standards can easily confuse you, and determining when annealed brass is necessary is another common consideration in CNC brass machining projects.
This article will help you distinguish between different brass grading systems and key grade properties, offer practical advice to avoid common application mistakes, and share a real case study at the end showing how our factory helped a customer resolve issues regarding lead-free requirements for water valve components, thread micro-cracks under load, and potential surface discoloration.
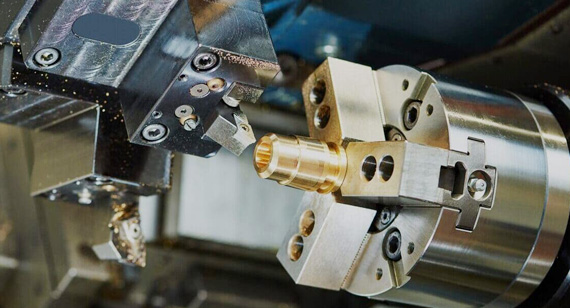
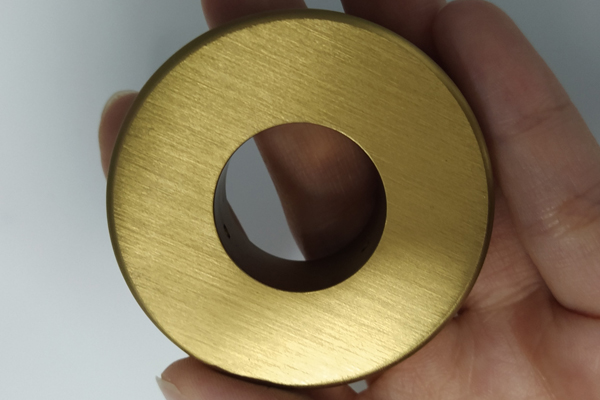
The US (ASTM) and European (EN) standards are the primary mainstream designation systems used internationally for brass materials, providing unified engineering benchmarks across global supply chains. As an essential material for CNC machining, brass is indispensable due to its unmatched combination of high machinability, excellent thermal conductivity, and natural corrosion resistance.
Below is a detailed comparison table mapping key European (EN) and US (ASTM) brass grades commonly specified in precision CNC machining:
| European Standard | US Standard | Core Chemical Composition | Strength / Fracture Resistance Rating | Elasticity Rating | Corrosion Resistance Rating | Impact Resistance Rating | Relative Part Machining Cost | Lead Content | CNC Machining Time |
| CuZn39Pb3 (CW614N) | C36000 | Cu 57-59%, Pb 2.5-3.5%, Zn Bal. | ★★★☆☆ | ★★☆☆☆ | ★★★☆☆ | ★★☆☆☆ | Low | Yes | Fast |
| CuZn39Pb2 (CW612N) | C37700 | Cu 57-59%, Pb 1.6-2.5%, Zn Bal. | ★★★☆☆ | ★★★☆☆ | ★★★☆☆ | ★★★☆☆ | Moderate | Yes | Fast |
| CuZn36Pb3 (CW603N) | C36000 (Equivalent Class) | Cu 60-62%, Pb 2.5-3.5%, Zn Bal. | ★★★☆☆ | ★★★☆☆ | ★★★☆☆ | ★★☆☆☆ | Low | Yes | Fast |
| CuZn30 (CW505L) | C26000 | Cu 69-71%, Zn Bal. | ★★☆☆☆ | ★★★★★ | ★★★★☆ | ★★★★☆ | High | No | Slow |
| CuZn37 (CW508L) | C27200 | Cu 62-64%, Zn Bal. | ★★★☆☆ | ★★★★☆ | ★★★☆☆ | ★★★☆☆ | Moderate-High | No | Average |
| CuZn38As (CW511L) | C27450 / Eco Brass | Cu 62-64%, As 0.02-0.15%, Zn Bal. | ★★★☆☆ | ★★★☆☆ | ★★★★★ (DZR) | ★★★☆☆ | Moderate-High | No (Lead-Free) | Average |
| CuZn31Si1 (CW708R) | C69300 / C69400 | Cu 75-77%, Si 0.8-1.2%, Zn Bal. | ★★★★☆ | ★★★☆☆ | ★★★★★ | ★★★☆☆ | High | No (Lead-Free) | Average |
| CuZn35Ni2Al1Fe1-B (CW710R) | C46400 (Naval Brass) | Cu 59-62%, Sn 0.5-1.0%, Zn Bal. | ★★★★☆ | ★★★☆☆ | ★★★★★ (Marine) | ★★★★☆ | Moderate-High | Trace / Optional | Average |
Grade Selection Recommendations for Common Brass Parts; According to Main Properties.
High-Precision Turned Parts and Fasteners (e.g., Screws, Nuts, Connectors)
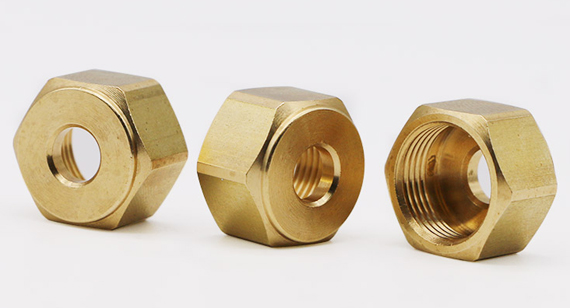
Potable Water Components and Medical Valves (e.g., Valve Bodies, Pipe Fittings)
Parts Requiring Secondary Bending or Crimping (e.g., Rivets, Terminal Pins)
Marine Hardware and High-Corrosion Components (e.g., Shafts, Marine Fittings)
Why You Should Care About Lead Content in Brass
Lead has traditionally been added to brass to act as an internal lubricant and chip breaker, giving standard alloys like C36000 exceptional machinability. However, strict environmental and health regulations across North America and Europe now place heavy restrictions on lead levels in components touching potable water, medical equipment, and consumer goods.
Failing to account for these compliance standards during material selection can result in severe commercial fallout. If your parts exceed legal lead thresholds, they risk failing certification, face immediate import rejections at customs, or trigger costly product recalls in target markets. To avoid these expensive pitfalls, components exporting to Western markets need to be carefully evaluated whether these parts are made by certified lead-free alternatives—such as C27450 or Eco Brass.
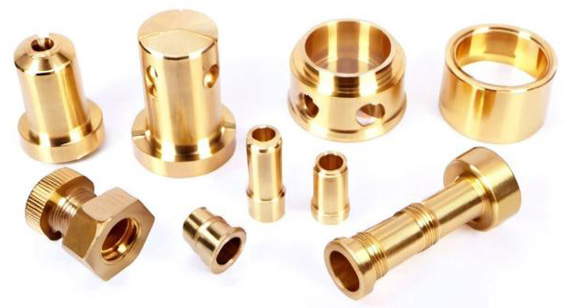
Can Free-Machining Brass Bring You Lower Costs and Faster Lead Times?
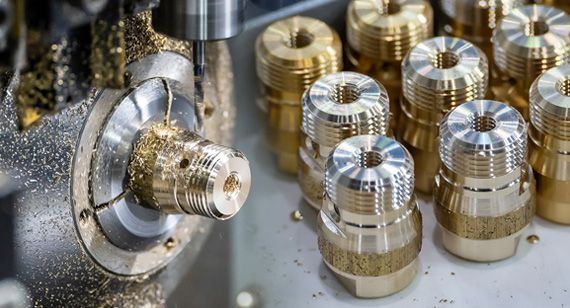
Yes. Free-machining brass, most notably C36000 and its European equivalent CuZn39Pb3, is renowned in precision manufacturing for reducing cycle times and driving down your production costs. This is because the lead particles distributed throughout the alloy act as microscopic chip breakers and internal lubricants, CNC machines can run at significantly higher spindle speeds and feed rates. The resulting small, brittle chips clear away effortlessly from the cutting zone, minimizing machine downtime, extending tool life, and delivering exceptional surface finishes straight off the machine without extra post-processing steps.
But there are also limitations that you need to focus on: The very lead additives that make these alloys so easy to cut also introduce internal stress points, which reduce overall ductility and impact strength, making them prone to cracking if subjected to heavy cold-forming, crimping, or high-vibration stress. Furthermore, as environmental regulations tighten around lead content, opting for free-machining brass in non-compliant applications can lead to regulatory bottlenecks.
Brass naturally tarnishes over time when exposed to oxygen, atmospheric moisture, sulfur compounds, and human touch. This chemical reaction creates a surface layer of copper oxide or patina, turning the bright golden finish into a dull, darkened, or brownish surface that can compromise both appearance and precise dimensional tolerances. You can ask for the following handling or surface treatment services to reolve the tarnish issue:
Requesting stress-relief annealing is worth considering for thin-walled brass parts, precision threaded components, or parts operating under high stress.
Even with gentle feed rates and specialized workholding, the initial rough machining phase, which removes the bulk of the material, inevitably generates hidden internal residual stresses. If these unreleased stresses remain inside the metal before final precision machining, thin walls can warp after being unclamped from fixtures, and precision threads are far more susceptible to micro-cracking when tightened under load. Performing a stress-relief annealing cycle after roughing stabilizes the material structure, ensuring critical dimensions hold tight tolerances and preventing premature stress corrosion cracking (SCC) in the field.
Because annealing is a secondary heat treatment process, it is often not included in standard CNC machining quotes and incurs an extra cost based on furnace batch volume. In terms of lead time, adding an annealing step typically extends production by 1 to 3 business days. While it introduces a modest fee and a short delay, specifying stress-relief annealing after roughing for high-precision or thin-walled brass parts is a smart safeguard against unexpected warping, assembly failures, and costly quality claims.
In the first section of this article, we introduced the primary US (ASTM) and European (EN) standard systems for CNC machining brass, breaking down common grades and offering initial application suggestions based on their core properties. Here, we take a more holistic approach, synthesizing operating environments, mechanical demands, regulatory compliance, and overall manufacturing economics into a unified decision framework to guide your final material selection.
| Operating Scenario | Recommended Brass Grade (ASTM / EN Equivalent) | Key Functional Advantages | Tarnishing / Oxidation Risk | Is Stress-Relief Annealing Recommended? | Relative Total Production Cost |
| General Precision Components and Fast-Turn Automation | C36000 / CuZn39Pb3 | 100% machinability rating, lowest tool wear, maximum cutting speeds. | Moderate (Requires basic packaging/passivation) | Only for delicate, thin-walled geometries | Low |
| Potable Water, Food Contact and Medical Devices | C27450 / C69300 (Eco Brass) | Fully compliant with NSF 61, RoHS, and EU drinking water lead-free regulations. | Low to Moderate | Recommended for complex liquid-channel manifolds | Moderate to High |
| Secondary Cold-Forming, Crimping, or Riveting | C37700 / CuZn39Pb2 | Enhanced ductility and elongation properties; resists cracking during cold deformation. | Moderate | Strongly recommended after rough machining/cold working | Moderate |
| Marine Environments and High-Corrosion Chemical Exposure | C46400 (Naval Brass) | Added tin content prevents dezincification and saltwater attack. | Low (Forms stable protective oxide layer) | Recommended prior to final thread finishing | Moderate to High |
| High Wear, Structural Loads, or High-Stress Applications | C69300 / Silicon Bronze Alternatives | Superior yield strength, hardness, and wear resistance compared to standard brass. | Low | Recommended for high-precision, load-bearing parts | High |
When making your final material decision, always let regulatory compliance and the operating environment drive your choice first. When the component is exported to North America or Europe and touches drinking water, food, or skin, non-leaded grades like C27450 are mandatory regardless of the slight increase in machining cycle times. Conversely, for non-regulated structural fasteners, industrial fittings, or electrical hardware, high-lead free-machining alloys like C36000 remain the most cost-effective choice.
Finally, consider the total manufacturing workflow rather than brass properties and costs alone. While specialized grades or lead-free alloys may increase initial material expenditure and tool wear, pairing them with appropriate secondary steps, such as passivation to prevent tarnishing or stress-relief annealing after roughing for delicate parts, will significantly reduce part failure rates and costly product recalls.
How We Resolved Lead Compliance, Thread Micro-Cracking, and Tarnishing Issues in CNC Machined Brass Water Valve Components.
A European plumbing industry client contacted our factory requesting custom CNC machined brass valve bodies for residential potable water supply lines. The component features fine internal threads (M22×1.5) and thin-walled fluid channels (1.8 mm wall thickness). Because the client's previous supplier purchased raw materials without strict certification, test batches failed to pass NSF/ANSI 61. Furthermore, under pressure testing at 1.6 MPa and a higher 2.5 MPa, micro-cracks propagated along the roots of the internal threads on the brass components, and components stored for over four weeks during transit developed localized dark spots and dull tarnishing.
To meet strict qualification standards, our engineering team executed a rigorous raw material control system, utilizing certified C27450 brass and reverifying every incoming batch in-house. Addressing the issue of thread micro-cracking, our engineers determined that high cutting forces during rough thread machining induced residual stress concentration along the 1.8 mm thin walls. We resolved this by optimizing cutting parameters and employing specialized thread-milling tools, while implementing a low-temperature stress-relief annealing process at 280°C for 90 minutes after rough machining. This eliminated internal stresses, preventing potential deformation during final finishing and mitigating the risk of micro-cracks forming under subsequent pressure testing environments.
To resolve surface oxidation and tarnishing of the brass valve body components, we used the automated multi-stage ultrasonic wash followed by a citric-acid passivation treatment. This effectively removed free surface copper ions and formed a uniform passive oxide barrier, significantly enhancing the components' corrosion resistance. Immediately after drying, the CNC machined brass valve bodies were sealed in VCI (Vapor Corrosion Inhibitor) bags containing desiccant packs, creating a protective environment that seals out ambient moisture, oxygen, and atmospheric pollutants during long-distance freight (a vital requirement for ocean transit).
The optimized valve housings passed 100% of independent laboratory testing for NSF/ANSI 61 and EU Drinking Water Directive compliance on the very first batch. Hydrostatic pressure testing achieved 2.5 MPa, with zero micro-cracking or pressure drop across 24-hour hold tests, while accelerated environmental testing estimated 24+ months of tarnish-free shelf life with less than a 7% total unit cost increase.
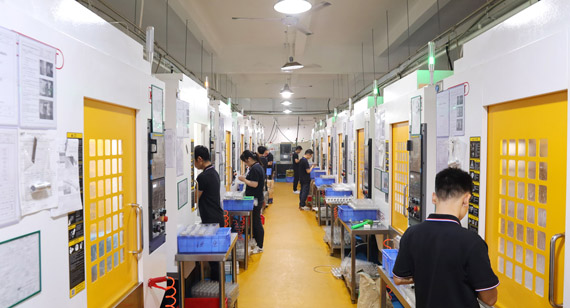
Successful brass CNC machining requires balancing material selection, regulatory compliance, structural design, and post-processing. While free-machining grades like C36000 provide rapid cycle times and cost efficiency for standard hardware, high-stakes applications demand a broader engineering view. Exporting or importing water-contact brass components to European and American regions mandates certified lead-free alloys to ensure strict environmental compliance. Furthermore, managing internal stress through post-roughing annealing prevents thin-wall warping and thread micro-cracking, while chemical passivation and VCI packaging prevent shipping-induced surface tarnishing. By addressing material properties, processing workflows, and environmental exposure early in the design stage, you can achieve optimal part performance while preventing expensive re-spins and quality recalls.
Navigating brass alloy standards, lead-free compliance, surface handling, and specialized heat treatment processes can be complex. Contact our engineering team for a free DFM review and instant quote, and we will help you select the exact brass grade and post-machining workflow tailored to the specific quality, regulatory, and cost requirements. [2D Drawings (PDF files), 3D Drawings (IGS/STP/STEP files)].
Send your 2D drawings, 3D CAD models, brass grade, compliance requirements, wall thickness, thread details, critical tolerances, surface finish, prototype quantity and production quantity. VMT will review material selection, DFM, machining process, post-processing and quotation requirements.
All information and uploaded files are secure and confidential.
1 Tell us what you need
2 Get solution & quote
3 Approve production
Email: inquiry@vimetal.com.cn
Does brass stick to tools and cause poor surface finish?
Free-machining brass and other leaded brasses rarely stick to tools due to the self-lubricating effect of lead, offering fast cutting performance and lower machining costs. However, softer, lead-free, or high-copper alloys (such as C27450, C46400, or C26000) are indeed more prone to tool sticking, resulting in surface qualities that require subsequent post-processing. Therefore, to prevent tool adhesion, machining suppliers will reduce feed rates, switch to specialized polished-rake carbide end mills, and maintain a continuous flow of coolant. These adjustments extend machining cycle times and increase tool wear, thereby raising your overall unit production cost.
How should I choose between silicon bronze and brass for CNC parts?
Choose brass (such as C36000 or C27450) for general-purpose applications where high machinability, tight tolerances, moderate corrosion resistance, and cost efficiency are paramount. Opt for silicon bronze, such as C69300 / C87600, when your application demands higher yield strength, superior wear and friction resistance, or enhanced fatigue performance under heavy structural loads and aggressive marine environments.
How do I distinguish between brass, bronze, and copper?
The key differences among brass, bronze, and copper are:
Are polishing and brushing common surface finishing processes for CNC brass parts? What effects do they achieve?
Yes, both are widely used post-machining finishes for brass components:
What processes should I request from the factory to prevent my brass parts from rusting?
While brass does not rust like steel, it oxidizes and tarnishes over time. Request citric-acid passivation to strip surface impurities and build a protective oxide film, or apply clear lacquer/electro-coating to seal out moisture and skin oils. For harsh outdoor environments, specify nickel plating, and request VCI anti-corrosion vacuum packaging for transit.
What are the key Design for Manufacturability (DFM) rules when designing CNC brass parts?
To minimize machining cycle times and tool wear, design internal radii to be at least 1/3 of the cavity depth so standard end mills can be used without excessive chatter. Avoid wall thicknesses below 1.0 mm to prevent part deformation under cutting forces, and specify standard thread sizes (such as M3 to M12 or standard NPT/G threads) to allow off-the-shelf tapping or thread-milling tools.
The technical information and manufacturing advice shared on the VMT website are for general guidance only. While we strive for accuracy, VMT does not guarantee that the processes, tolerances, or material properties mentioned are applicable to every specific project. Any reliance you place on such information is strictly at your own risk. It is the buyer's responsibility to provide definitive engineering specifications for any production orders. Final specifications and service terms shall be subject to the formal contract or quotation confirmed by both parties.


 +86 15099911516



 Read more