16 years one-stop China custom CNC machining parts factory
Hey there I’m VMT Sam!
With 25 years of CNC machining experience we are committed to helping clients overcome 10000 complex part-processing challenges all to contribute to a better life through intelligent manufacturing. Contact us now
 437 |
Published by VMT at Sep 17 2026 | Reading Time:About 6 minutes


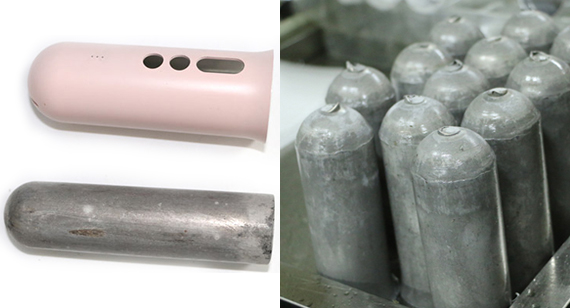
Die casting and injection molding are two highly cost-effective manufacturing processes widely used in automotive, medical, consumer electronics, and industrial design sectors. Everyday items such as plastic toys, plastic side-mirror housings for cars, various plastic enclosures for medical devices, and plastic protective covers for large industrial equipment are most commonly produced through plastic injection molding. On the other hand, hardware, laptop stands, camera bodies, and toys made from low-melting-point non-ferrous metals and alloys, such as aluminum, zinc, magnesium, and copper, are predominantly manufactured using die casting.
By leveraging custom tooling and molds, both die casting and injection molding serve as excellent options for scaling up your custom part production. Choosing the right manufacturing process directly impacts product performance and budget success. This guide will thoroughly explain how each process works, compare their tolerances, surface finishes, costs, applications, and ultimately help you determine which process best suits your project's production needs.
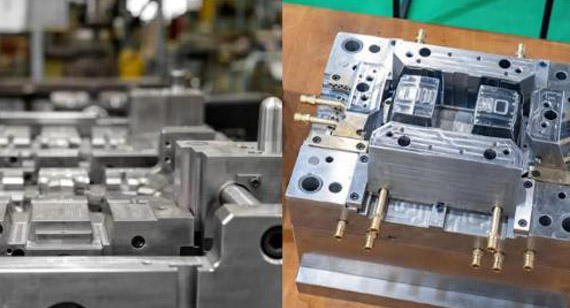
At the end of this article, we will also share a case study on how our factory combined die casting with secondary CNC machining and surface finishing. This approach enabled us to cost-effectively (28% reduction) produce heat sink housings for new energy vehicles while meeting strict requirements for high thermal conductivity, high strength, high-temperature resistance, and tight tolerances of ± 0.015mm.
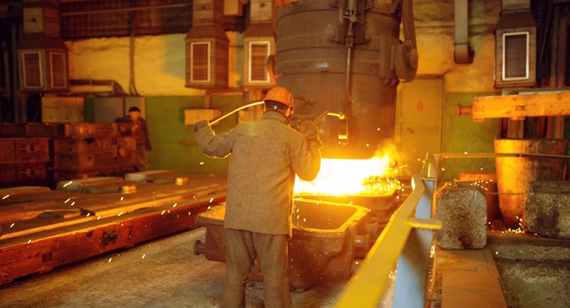
Die casting is a high-pressure metal fabrication process engineered for manufacturing high-precision, non-ferrous metal components with complex geometries.
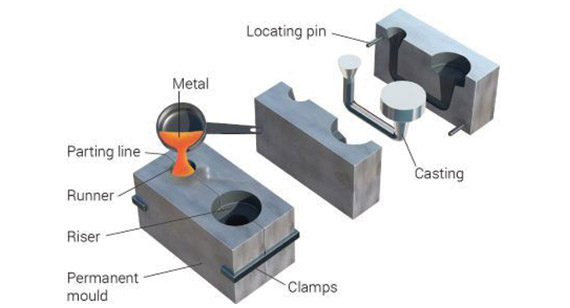
How the Process Works
Primary Material Options and Processing Constraints
Plastic injection molding is the standard high-volume manufacturing method for custom thermoplastic components, renowned for high repeatability and surface consistency.
How the Process Works
Core Value and Design Strengths
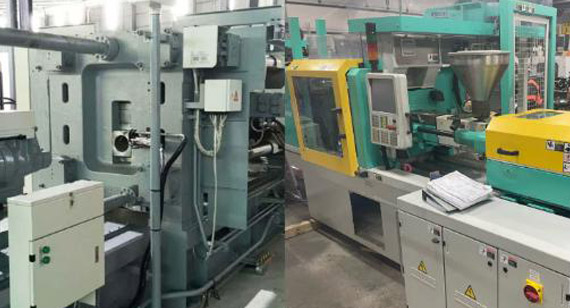
While both processes rely on high-pressure injection into custom tooling, choosing between die casting and plastic injection molding comes down to material capabilities, structural tolerances, tooling investment, and surface finishing requirements.
The comparison table below breaks down the primary technical and economic differences to help you select the right manufacturing method for your production volume.
| Dimension | Die Casting | Injection Molding |
| Primary Materials | Non-ferrous metals (low melting point alloys: Aluminum, Zinc, Magnesium, Copper/Brass) | Thermoplastics (ABS, PC, Nylon/PA, POM, PP, PE, PEEK, etc.) |
| Material Limitations | Not suitable for high melting point metals (e.g., steel, iron) | Not suitable for thermosetting plastics or non-meltable materials |
| Precision and Tolerances | ±0.02 mm to ±0.05 mm (High structural rigidity, predictable thermal shrinkage) | ±0.1 mm to ±0.2 mm (Standard); down to ±0.05 mm for engineering resins (influenced by shrinkage and warpage) |
| Geometric Complexity | Ideal for intricate shapes; overly large parts are not suitable | Ideal for complex, fine features, thin walls, and snap-fits |
| Surface Finish Quality | Ra 1.6 μm to 3.2 μm (Smooth raw cast finish; easily enhanced by shot blasting or polishing) | Ra 0.4 μm to 1.6 μm (High gloss out of mold); supports SPI/VDI textures and fine graining |
| Common Defect Risks | Air porosity (trapped gas bubbles inside metal) | Sink marks, warpage, flash, and flow lines |
| Cost Efficiency and Volume | Tooling costs are very high; highly cost-effective for large production runs | High initial tooling cost (generally lower than metal dies); exceptional cost efficiency at scale (100k+ units) |
| Post-Processing and Surface Treatments | Anodizing, electroplating, powder coating, passivation, shot blasting | Gate removal, flash trimming, cleaning, painting, pad printing, silk screening |
Precision and Dimensional Tolerances
Surface Finish and Cosmetic Capability
Common Defect Risks and Design Mitigations
Tooling Investment and Cost Efficiency
Selecting the right raw material is crucial to balancing mechanical performance, thermal properties, and total manufacturing costs.
Common Die Casting Metals
Common Injection Molding Thermoplastics
Both processes yield ready-to-use parts directly out of the mold, but distinct secondary operations are often required based on aesthetic, tolerance, or functional demands.
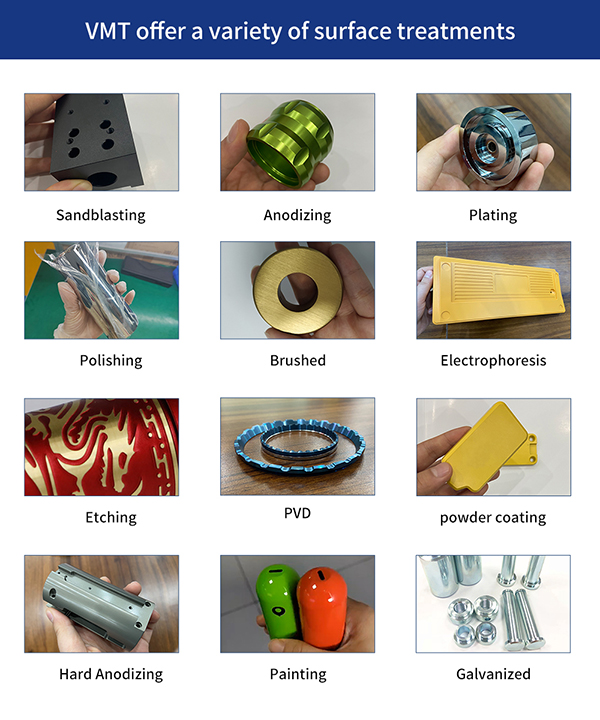
Die Casting Finishing and Secondary Processing
Because cast metals often retain runner marks, flash, or minor surface imperfections, die-cast parts frequently require post-processing:
Injection Molding Finishing and Secondary Processing
Plastic components typically exit the mold with smooth, fine textures, significantly reducing extra finishing costs:
Automotive and New Energy Vehicles (NEVs)
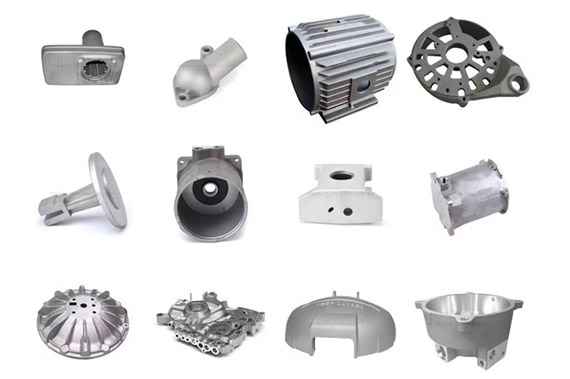
Die Casting Choice: Structural battery pack housings, powertrain brackets, and motor heat sink enclosures (ADC12 / A380 Aluminum).
Rationale: Metals provide the necessary heat dissipation, high structural integrity, and resistance to elevated engine temperatures. Die casting allows complex, thin-walled heat sink fins to be cast in a single shot, achieving tighter structural tolerances than plastic molding.
Injection Molding Choice: Interior dashboard components, door handles, and exterior side-mirror covers (PC+ABS, Nylon).
Rationale: Thermoplastics lower total vehicle weight to improve range/fuel efficiency, provide excellent surface finishes straight out of the tool, and reduce tooling costs for interior trim options.
Consumer Electronics and Smart Devices
Die Casting Choice: Internal frame chassises, camera bodies, and laptop structural hinges (ZAMAK Zinc, AZ91D Magnesium).
Rationale: Zinc and magnesium alloys provide rigid structural support, natural EMI/RFI shielding, and ultra-thin wall capabilities while keeping hand-held devices sturdy.
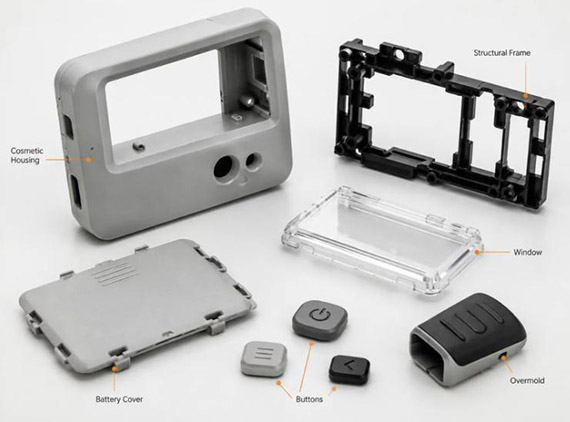
Injection Molding Choice: Smart TV bezels, smartphone cases, and wearable tech enclosures (PC, ABS).
Rationale: Delivers lightweight insulation, complex internal snap-fit geometry, and smooth tactile surfaces. At high production runs (10,000+ units), unit costs become exceptionally low.
Die Casting Choice: Main motor mounts, central flight controller housings, and heavy-load landing gear brackets (Magnesium / Aluminum).
Rationale: Provides the maximum strength-to-weight ratio needed to survive high-impact landings and vibration stresses while keeping critical mounting points rigid.
Injection Molding Choice: Protective top covers, propeller guards, and quick-release battery compartments (Nylon/PA, POM).
Rationale: Keeps non-structural parts extremely light to maximize flight time while retaining impact flexibility to prevent cracking during collisions.
Die Casting Choice: Base plates for heavy equipment, surgical monitor mounting arms, and portable ultrasound chassis.
Rationale: Offers heavy-duty stability, high load-bearing capacity, and compatibility with chemical sterilization coatings.
Injection Molding Choice: Disposable syringes, medical device housings, fluid connectors, and test tube racks (Medical-grade PC, PP, PEEK).
Rationale: Ensures precise fluid channel geometry, and cleanroom-compatible high-volume production.
Manufacturing High-Performance NEV Heat Sink Housings
As the new energy vehicle (NEV) market rapidly expands, thermal management systems face increasingly stringent performance standards. A leading automotive client approached our factory to manufacture a specialized heat sink housing.
The component demanded exceptional thermal conductivity to dissipate power module heat, high structural strength to withstand road vibrations, superior high-temperature resistance, and ultra-tight tolerances for fluid-tight sealing. Producing this part through CNC machining alone was cost-prohibitive, while standard die casting could not achieve the required dimensional precision on critical mating surfaces. To solve this challenge, our engineering team used a hybrid manufacturing approach that integrated high-pressure aluminum die casting with precision secondary CNC machining.
First, we utilized ADC12 aluminum alloy to cast the core housing structure and thin-walled cooling fin arrays in a single, high-efficiency shot. This optimized material flow and allowed us to achieve the intricate geometry needed for maximum heat dissipation, drastically reducing material waste and initial cycle times compared to machining solid billet blocks.
Following the initial casting, the housings underwent secondary CNC machining on selected critical surfaces. While die casting formed the complex heat sink fins, our multi-axis CNC machines milled the O-ring sealing grooves, mounting flanges, and threaded holes to precise tolerances of ±0.015 mm. This targeted machining step avoided the risk of liquid coolant leaks and ensured perfect alignment during vehicle assembly, without incurring the high costs of fully machining the entire housing geometry.
Finally, the components underwent a specialized surface finishing process involving shot blasting and chemical passivation. This combination removed micro-burrs, improved surface uniformity, and created a corrosion-resistant protective layer without compromising thermal performance. By effectively combining raw die casting efficiency, targeted CNC precision, and protective surface treatments, our factory delivered a scalable, cost-effective solution that met all automotive-grade performance standards while cutting per-unit production costs by 28%.
Choosing between die casting and plastic injection molding ultimately comes down to your part's mechanical demands, operating environment, and target production volume. While injection molding provides unmatched cost efficiency, light weighting, and versatile surface finishes for plastic components, die casting remains the premier choice when high thermal conductivity, structural strength, and EMI shielding are required. Partnering with an on-demand manufacturing supplier that offers both primary casting/molding and advanced secondary CNC machining ensures your components achieve optimal precision at the lowest per-unit cost. Have a challenging part design or unsure which process best fits your budget and specs? Contact our engineering team to receive a free design-for-manufacturability (DFM) analysis and a competitive quote for your custom production needs. [2D Drawings (PDF files), 3D Drawings (IGS/STP/STEP files)].
Send your 2D drawings, 3D CAD models, material requirements, target tolerances, surface-finish requirements, prototype quantity and production volume. VMT will review manufacturability, process selection, secondary CNC machining, finishing and quotation requirements.
All information and uploaded files are secure and confidential.
1 Tell us what you need
2 Get solution & quote
3 Approve production
Email: inquiry@vimetal.com.cn
Is die casting tooling more expensive than plastic injection molding tooling?
Yes, die casting molds are typically 20% to 30% more expensive than plastic injection molds. Metal dies must be constructed from heavy-duty, heat-resistant tool steels (such as H13) to withstand high injection pressures and extreme thermal shock from molten metals, whereas plastic injection molds experience lower operational temperatures which often use P20 steel, 718 steel, or 7075 aluminum.
Can plastic injection molding replace die casting to save weight?
Plastic injection molding can replace metal die casting if the structural load, operating temperature, and thermal conductivity requirements are low. Engineering thermoplastics like PEEK or glass-filled Nylon offer high strength-to-weight ratios, but they cannot match the thermal dissipation or natural EMI shielding of metals like aluminum or magnesium.
What is the typical lifespan of a die casting mold vs. an injection mold?
A steel die casting mold typically lasts between 100,000 to 150,000 shots due to thermal fatigue and erosion caused by liquid metal. In contrast, a hardened steel plastic injection mold can easily exceed 1,000,000 cycles because melted polymers cause significantly less thermal wear and stress on the tool.
Why do die-cast parts often require secondary CNC machining while injection-molded parts do not?
Die-cast parts frequently require secondary CNC machining to achieve ultra-tight tolerances (e.g., ±0.015 mm) on critical mating surfaces, thread taps, and O-ring grooves, as well as to remove flash and runner gates. Injection-molded plastic parts exit the mold with high surface consistency and tight feature definition, usually requiring only minor gate trimming.
How do you prevent air porosity defects in aluminum die casting?
Air porosity can be minimized by optimizing mold flow design, using vacuum-assisted die casting to pull air out of the cavity before injection, controlling shot speeds, and maintaining proper overflow wells. For critical sealing applications, secondary CNC machining and vacuum impregnation sealing are also applied.
Can I perform anodizing or electroplating on both die-cast and injection-molded parts?
No, traditional anodizing and electroplating are surface treatments designed specifically for conductive metal parts like aluminum or zinc die castings. Plastic injection-molded parts cannot be anodized, though specialized plastic plating processes (like electroplated ABS) or vacuum metallization can apply decorative metal coatings to plastic surfaces.
The technical information and manufacturing advice shared on the VMT website are for general guidance only. While we strive for accuracy, VMT does not guarantee that the processes, tolerances, or material properties mentioned are applicable to every specific project. Any reliance you place on such information is strictly at your own risk. It is the buyer's responsibility to provide definitive engineering specifications for any production orders. Final specifications and service terms shall be subject to the formal contract or quotation confirmed by both parties.


 +86 15099911516



 Read more