16 years one-stop China custom CNC machining parts factory
Hey there I’m VMT Sam!
With 25 years of CNC machining experience we are committed to helping clients overcome 10000 complex part-processing challenges all to contribute to a better life through intelligent manufacturing. Contact us now
 445 |
Published by VMT at Nov 07 2026 | Reading Time:About 6 minutes


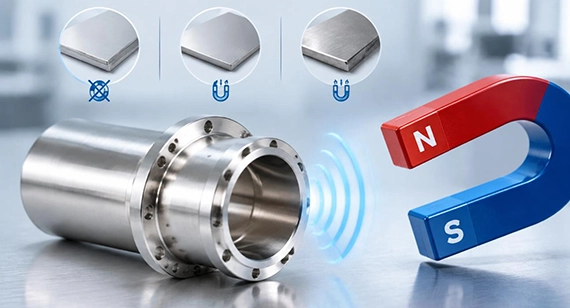
Not all stainless steel is magnetic. Its magnetic properties mainly depend on its metallurgical structure, specific grade, and processing condition. In general, austenitic stainless steels (such as 304, 316, and 316L) are typically non-magnetic or weakly magnetic in the annealed condition, while ferritic stainless steel (such as 430) and martensitic stainless steels (such as 410, 420, and 440C) are generally magnetic. In addition, austenitic stainless steels such as 304 may develop some magnetism after cold working, bending, or significant mechanical deformation due to strain-induced martensite formation. For CNC precision stainless steel parts, magnetism is relevant to material selection, machining processes, and final application requirements. For example, MRI equipment, precision sensors, and other devices sensitive to magnetic fields require particular attention to the material's relative magnetic permeability.
Overview
This article explores the magnetic properties of different stainless steel grades, their implications for CNC machining, and key considerations for material selection and quality control when designing and sourcing precision stainless steel parts. At the end, we also share a case study in which our CNC machining factory helped a customer resolve weak magnetism in the thin-wall edge areas of a stainless steel sensor housing for imaging equipment, which posed a risk of signal drift. The solution achieved a relative magnetic permeability of μr ≤ 1.01 while meeting the customer's requirements for an assembly tolerance of ±0.01 mm and a surface roughness of Ra 0.6 μm.
Whether a specific stainless steel grade exhibits magnetism depends primarily on its crystal lattice structure and chemical composition, rather than its chromium content or corrosion resistance alone.
At the microscopic level, magnetism in ferrous alloys is governed by how iron atoms are arranged:
Therefore, stainless steel is not inherently "all magnetic" or "all non-magnetic"—its behavior is dictated by which phase dominates its metallurgical matrix:
Ferritic Stainless Steel
Ferritic stainless steel has a body-centered cubic (BCC) crystal structure and is generally magnetic. It offers good strength and corrosion resistance, although its corrosion resistance and mechanical properties vary by grade. Common examples include 430 stainless steel.
Martensitic Stainless Steel
Martensitic stainless steel has a body-centered tetragonal (BCT) or related martensitic structure formed through heat treatment. It is magnetic and can achieve high hardness and strength through quenching and tempering. Common grades include 410, 416, 420, and 440C.
Austenitic Stainless Steel
Austenitic stainless steel has a face-centered cubic (FCC) crystal structure and is generally non-magnetic or weakly magnetic in the annealed condition. It offers good corrosion resistance, toughness, and ductility. Common grades include 303, 304, 304L, 316, and 316L. However, cold working and machining-induced deformation may increase magnetism in some grades due to strain-induced martensite formation.
Other Stainless Steel Types
In addition to austenitic, ferritic, and martensitic stainless steels, there are also duplex and precipitation-hardening (PH) stainless steels. Duplex stainless steels, such as 2205 and 2507, contain both austenitic and ferritic phases and are generally magnetic. Precipitation-hardening grades, such as 17-4 PH (630), are also generally magnetic due to their martensitic or semi-austenitic metallurgical structures, depending on the grade and heat treatment condition.
Table: Grades & Magnetic Properties of Common CNC Machiend Stainless Steel
| Grade | Structure | Raw Magnetism (Annealed Condition) | Post-CNC Machining Magnetism |
| 304 | Austenitic | Generally non-magnetic or weakly magnetic | May develop increased magnetism due to strain-induced martensite from machining or cold working |
| 304L | Austenitic | Generally non-magnetic or weakly magnetic | May develop some magnetism under significant cold deformation |
| 316 | Austenitic | Generally non-magnetic | May develop weak magnetism after significant cold working or machining deformation |
| 316L | Austenitic | Generally non-magnetic | Usually maintains low magnetic response, but some magnetism may develop after deformation |
| 303 | Austenitic | Generally non-magnetic or weakly magnetic | May exhibit some magnetism depending on material condition and machining deformation |
| 430 | Ferritic | Magnetic | Remains magnetic after CNC machining |
| 410 | Martensitic | Magnetic | Remains magnetic; heat treatment may change its magnetic response |
| 416 | Martensitic | Magnetic | Remains magnetic |
| 420 | Martensitic | Magnetic | Remains magnetic |
| 440C | Martensitic | Magnetic | Remains magnetic |
| 2205 | Duplex | Magnetic | Generally remains magnetic |
| 2507 | Super Duplex | Magnetic | Generally remains magnetic |
| 17-4 PH (630) | Precipitation-Hardening | Magnetic | Generally remains magnetic; depends on heat treatment condition |
Note: Magnetic behavior varies with chemical composition, heat treatment, cold working, and machining conditions. The descriptions above are general material characteristics, not guaranteed magnetic specifications. For applications requiring strict low-magnetic properties, specify a maximum relative magnetic permeability (μr) and verify it through appropriate testing.
Magnetic requirements vary across applications. When selecting materials for CNC machined parts, design engineers and procurement teams should consider the actual operating environment, mechanical properties, and magnetic requirements of each component.
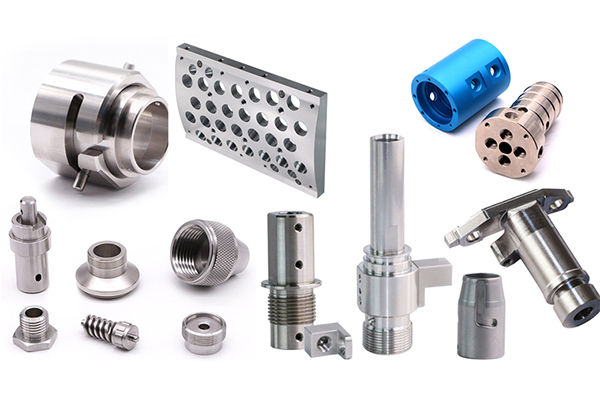
In precision CNC machining and critical applications, such as medical imaging and aerospace sensors, simple qualitative observations are often insufficient. The quality control teams use different inspection methods depending on the required magnetic sensitivity and engineering specifications.
1. Permanent Magnet Test (Rough Workshop Screening):
A quick, non-destructive screening method using a handheld neodymium magnet. It helps distinguish strongly magnetic ferritic and martensitic stainless steels from typically non-magnetic austenitic grades. However, austenitic stainless steels such as 304 and 316 can develop weak localized magnetism due to cold working, machining deformation, or the formation of strain-induced martensite. This test cannot quantify residual magnetism or determine relative magnetic permeability.
2. Gaussmeter / Hall Effect Sensor (Surface Residual Magnetism):
A gaussmeter equipped with a Hall effect probe measures the magnetic flux density near machined surfaces, thin walls, edges, and corners, typically in Gauss or Tesla. This method helps identify localized residual magnetic fields that may attract ferrous particles or interfere with nearby magnetic-sensitive components. For consistent results, measurement locations, probe orientation, and sensor distance should be controlled. It is important to note that surface magnetic field measurements do not directly determine the material's relative magnetic permeability.
3. Magnetic Permeability Indicator (ASTM A342/A342M Compliance):
For applications with strict magnetic requirements, relative magnetic permeability (μr) provides a quantitative basis for evaluating weakly magnetic materials. Low-Mu Permeability Indicators can compare a material's permeability against calibrated reference standards, while fluxmetric methods and vibrating sample magnetometry (VSM) provide other measurement approaches covered by ASTM A342/A342M. You can use these methods to evaluate whether austenitic stainless steel components meet specified magnetic requirements after machining or heat treatment. Depending on the application, engineering acceptance limits may include μr ≤ 1.02 or μr ≤ 1.01. These values should be defined by the customer's specifications rather than treated as universal ASTM acceptance limits.
Austenitic stainless steels such as 304 are generally non-magnetic in the annealed condition. However, CNC milling, turning, and other machining operations can introduce significant mechanical stress and plastic deformation, potentially transforming some austenite into magnetic martensite. This phenomenon is known as strain-induced martensite formation.
This transformation is often accompanied by work hardening, which can increase local hardness and affect subsequent machining operations. The degree of magnetic change depends on the material grade, initial condition, and extent of deformation.
To reduce or eliminate this effect, several measures can be considered:
Note: If a CNC machined part has strict magnetic permeability requirements, specify the maximum allowable relative magnetic permeability (μr) on the drawing and verify it after machining and any subsequent heat treatment.
Magnetism does not usually directly determine CNC machining accuracy, but different stainless steel structures have different machining characteristics and fixturing requirements, which can affect machining stability, dimensional accuracy, and surface quality.
1. Fixturing
Ferritic and martensitic stainless steels (such as 430, 410, and 416) are magnetic and can be held using magnetic chucks in suitable machining operations. Austenitic stainless steels (such as 304 and 316L), which are generally non-magnetic or weakly magnetic, require mechanical vises, custom soft jaws, or dedicated fixtures. For thin-wall parts, clamping force must also be properly controlled to prevent deformation.
2. Machinability & Surface Finish
Austenitic stainless steels are prone to work hardening. Improper cutting parameters or repeated tool rubbing against the workpiece can increase cutting forces and tool wear, affecting surface roughness. Sharp carbide tools, appropriate cutting parameters, and effective coolant delivery should be selected to maintain stable cutting conditions and ensure proper chip evacuation.
3. Machining Deformation & Magnetic Control
Austenitic stainless steels such as 304 may develop strain-induced martensite after significant plastic deformation, increasing local magnetism. For parts used in MRI equipment, precision sensors, and other low-magnetic applications, specify the material grade and maximum allowable relative magnetic permeability (μr) at the design stage. The machining factory should optimize the process based on the material condition and perform magnetic testing after machining.
A medical imaging equipment manufacturer approached us for a batch of custom 304 stainless steel sensor housings used in precision imaging equipment. After receiving parts machined by a previous supplier, the customer used a Gauss meter to inspect their magnetic properties and detected weak magnetism in the thin-wall edge areas. This raised concerns about potential interference with sensor signals and resulting imaging signal drift. Since the components had strict requirements for magnetic properties, assembly accuracy, and surface quality, the customer was looking for a new CNC machining supplier to resolve the issue.
After reviewing the component structure and the previous machining process, our engineering team determined that the problem was likely related to localized plastic deformation during cutting. The previous supplier's use of high-depth-of-cut, high-speed milling may have caused localized strain concentration, promoting deformation-induced martensitic transformation in the 304 austenitic stainless steel. As a result, areas that were originally weakly magnetic or nearly non-magnetic developed detectable weak magnetism.
To address the issue, we optimized both the machining process and post-machining treatments. First, we adjusted the cutting parameters by using shallow cuts, low feed rates, and high-pressure coolant to reduce heat accumulation and localized cutting stress. Second, we introduced vacuum solution annealing after machining, with appropriate control over the treatment temperature, holding time, and cooling method, to reduce the effects of deformation-induced martensite on magnetic properties. Demagnetization was also performed to further control residual magnetism. In addition, during the DFM review, we recommended that the customer consider upgrading the material to 316L for subsequent production batches. Although 316L generally has a lower carbon content and better corrosion resistance, its magnetic properties after machining still need to be verified based on the material condition and actual manufacturing process. It should not be regarded as an absolutely non-magnetic material.
As a result, the optimized components achieved a relative magnetic permeability of μr ≤ 1.01, while meeting the customer's requirements for an assembly tolerance of ±0.01 mm and a surface roughness of Ra 0.6 μm. This resolved the weak magnetism in the thin-wall edge areas while maintaining the required assembly precision and surface quality.
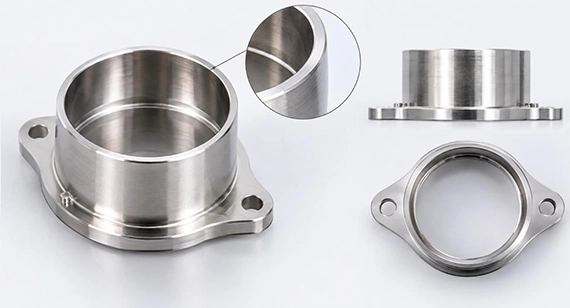
Whether stainless steel has magnetic properties depends on its chemical composition and crystal structure. Ferritic and martensitic stainless steels typically exhibit magnetic properties, while austenitic stainless steel has weak or no magnetic properties. Non-magnetic stainless steel is widely used in aerospace, medical devices, construction, and other fields. Understanding the magnetic properties of stainless steel is crucial for selecting suitable materials, optimizing processing techniques, and improving product quality.
As experts in the CNC machined parts manufacturing field, we offer customized non-magnetic stainless steel CNC machined parts services. We have advanced CNC machining equipment and a professional technical team capable of producing high-quality, high-precision non-magnetic stainless steel parts according to customer requirements. Our service range includes CNC prototyping machining, custom CNC machining, and more, aiming to meet customers' personalized needs.
Our non-magnetic stainless steel CNC machined parts services offer the following advantages:
Send your 2D drawings, 3D CAD models, stainless steel grade, magnetic permeability requirements, critical tolerances, surface roughness, heat-treatment requirements, prototype quantity and production quantity. VMT will review material selection, CNC machining strategy, magnetic-control requirements, inspection methods, finishing and quotation requirements.
All information and uploaded files are secure and confidential.
1 Tell us what you need
2 Get solution & quote
3 Approve production
Email: inquiry@vimetal.com.cn
Does magnetic stainless steel affect CNC machining precision?
Yes. Magnetic properties cause fine metal swarf to cling to the workpiece and end mill, potentially leading to chip re-cutting, premature tool wear, and degraded surface roughness (Ra).
Which stainless steel is best if my CNC parts strictly require zero magnetism?
Grade 316 or 316L. Due to higher nickel (10-14%) and molybdenum content, its austenite structure is significantly more stable and resistant to deformation-induced magnetism than 304.
How do you remove residual magnetism from machined stainless steel parts?
Through solution annealing (heating above 1050°C followed by rapid quenching) to restore the austenitic structure, or by using an industrial AC demagnetizer for temporary electromagnetic de-gauging.
Will solution annealing to eliminate magnetism distort my tight-tolerance CNC parts?
High-temperature solution annealing (typically 1,050°C–1,100°C) carries a risk of thermal stress relief and dimensional warping, particularly on thin-walled or asymmetrical geometries. To preserve tight tolerances (± 0.01 mm or better), precision machine shops often implement a two-stage process: rough machining → stress-relief/solution annealing in a vacuum furnace → final precision finishing passes to clean up critical datum planes and bearing journals.
Can I use free-machining 303 stainless steel if my part requires low magnetism?
While 303 is an austenitic grade offering exceptional machinability and lower cycle times, it is more susceptible to deformation-induced magnetism during heavy turning or milling than 316L. Additionally, its sulfur additives slightly degrade corrosion resistance. If zero-to-low permeability is an absolute engineering requirement, 316L remains the superior choice despite its tougher machinability.
Does passivation or electropolishing affect the magnetic properties of machined stainless steel?
Chemical passivation and electropolishing do not alter the bulk crystal structure or remove strain-induced martensite inside the material. However, electropolishing removes the micro-stressed surface layer created by tool shearing and eliminates free iron/debris, which can marginally reduce surface magnetic readings and optimize overall corrosion performance.
The technical information and manufacturing advice shared on the VMT website are for general guidance only. While we strive for accuracy, VMT does not guarantee that the processes, tolerances, or material properties mentioned are applicable to every specific project. Any reliance you place on such information is strictly at your own risk. It is the buyer's responsibility to provide definitive engineering specifications for any production orders. Final specifications and service terms shall be subject to the formal contract or quotation confirmed by both parties.


 +86 15099911516



 Read more