16 years one-stop China custom CNC machining parts factory
Hey there I’m VMT Sam!
With 25 years of CNC machining experience we are committed to helping clients overcome 10000 complex part-processing challenges all to contribute to a better life through intelligent manufacturing. Contact us now
 537 |
Published by VMT at Sep 30 2026 | Reading Time:About 6 minutes


6061 and 7075 aluminum are two well-known materials for CNC machining. The former features a good strength-to-weight ratio and is more common and economical in general industrial applications, such as 6061 aluminum heat sinks, electronic enclosures, automotive chassis, and drone brackets. The latter possesses a higher strength-to-weight ratio but comes at a higher cost, making it typically more common in high-performance racing, drones, or aerospace applications.
However, simply focusing on the basic properties and applications of 6061 vs. 7075 is far from enough. You wouldn't want to face unexpected color mismatched after anodizing due to choosing the wrong alloy or process, severe cracking risks caused by welding 7075, or thin-wall warping due to residual stress. Furthermore, knowing how to achieve good surface finish along with wear and corrosion resistance, and accounting for the resulting extra lead times and costs, demands equal attention.
This article aims to guide you through the main property differences between 6061 vs 7075, the hidden pitfalls and preventive measures regarding anodizing, welding, and deformation issues in engineering applications, as well as alternative surface finishing options and their impacts. At the end of this guide, we will also share a case study on how our machine shop advised an automotive client on selecting the right aluminum material and machining process for a suspension rocker part, achieving zero deformation and maintaining a precise ±0.03mm hole distance tolerance.
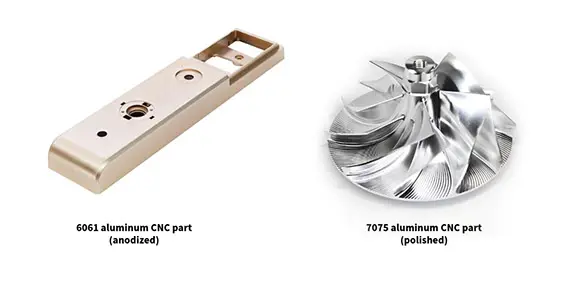
To put it this way, you cannot visually distinguish 7075 from 6061 aluminum alloy with the naked eye. Becasue they both present a similar silver-white metallic finish when they are not surface finished or polished. When it comes to physical properties, the differences between them are minor and fairly close.
The most pronounced differences lie in their mechanical properties. 7075 aluminum significantly outperforms 6061 in ultimate tensile strength, yield strength, and hardness. On the other hand, 6061 aluminum holds a slight edge in fracture toughness and elongation at break.
Physical and Mechanical Properties Table
Although you can look up these parameters across various engineering databases, we have compiled their typical values below for your quick engineering reference:
| Property | 6061-T6 | 7075-T6 | 7075-T651 |
| Density | 2.70 g/cm³ | 2.81 g/cm³ | 2.81 g/cm³ |
| Melting Point Range | 582 – 652 °C | 477 – 635 °C | 477 – 635 °C |
| Thermal Conductivity | 167 W/m·K | 130 W/m·K | 130 W/m·K |
| Coefficient of Thermal Expansion | 23.2 µm/m·°C | 23.6 µm/m·°C | 23.6 µm/m·°C |
| Ultimate Tensile Strength | ~310 MPa | ~572 MPa | ~570 MPa |
| Yield Strength | ~276 MPa | ~503 MPa | ~503 MPa |
| Hardness (Brinell) | 95 HB | 150 HB | 150 HB |
| Fatigue Strength | 96 MPa | 159 MPa | 159 MPa |
| Fracture Toughness | ~29 MPa·m1/2 | ~24 MPa·m1/2 | ~24 MPa·m1/2 |
| Elongation at Break | 12% | 11% | 11% |
| Controlled Stretch Ratio | 0% | 0% | 1.5% – 3.0% |
| Peak Residual Stress | ~80 – 120 MPa | ~150 – 220 MPa | < 20 – 30 MPa |
| Machining Distortion Risk | Moderate | Very High | Minimal |
Both 6061 and 7075 belong to the heat-treatable aluminum alloy category (classified by chemical composition by the Aluminum Association). This means they can achieve distinctly different mechanical performance levels through varying heat treatment combinations.
The table above highlights the most common tempers used in aluminum CNC machining:
However, selecting between 6061 and 7075 aluminum goes far beyond just evaluating their temper designations and mechanical datasheets. Next, let’s explore the common engineering traps and practical solutions when working with 6061 vs. 7075 aluminum.
In fact, for many CNC machined parts, such as drone brackets, gimbal structural components, bicycle pedals, handlebars, seatposts, motorcycle swingarms, and chainring mounts, both materials can be used. The 7075 aluminum version is simply more wear-resistant and resistant to deformation under pressure, while the 6061 aluminum version is cheaper and relatively more corrosion-resistant.
However, for aluminum parts that require Type II anodizing in bright colors, such as aluminum electronics enclosures, cooling devices, pedals with such aesthetic demands, or exterior parts for automobiles and drones, choosing 6061 aluminum is recommended.
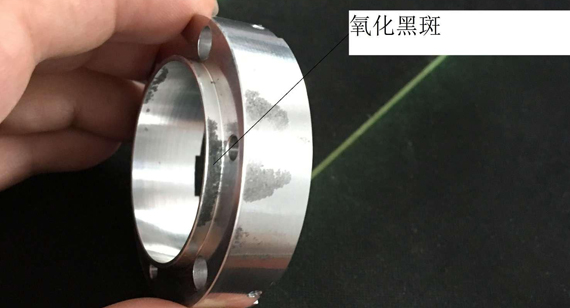
This is because 7075 aluminum alloy contains a higher proportion of zinc (5.1%-6.1%) and copper (1.2%-2.0%), whereas 6061 consists mainly of magnesium and silicon. During the anodizing process, the copper element affects the purity and transparency of the oxide film, causing the layer to easily turn grayish, yellowish, or mottled, resulting in a dull and inconsistent color after dye absorption.
This is just like when you want to produce a batch of royal blue electronics enclosures or bright red drone motor arms: using 6061 for anodizing produces highly saturated, vivid bright colors. But for the same parts machined by 7075 aluminun and use the exact same dyes, the final red part may appear dull and grayish, and the blue parts are prone to noticeable batch color variations.
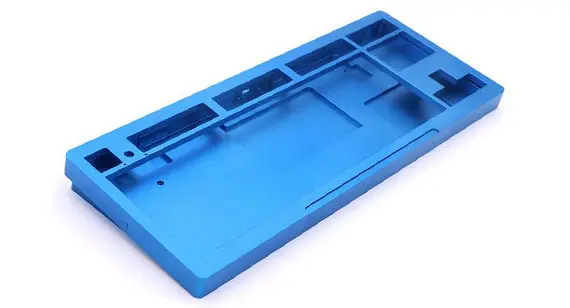
Furthermore, for these Type II anodized aluminum parts requiring bright colors, high strength and hardness are rarely core requirements, making it unnecessary to choose 7075 aluminum.
In cases where a part strictly requires 7075 aluminum and also demands accurate, bright colors, you need to work with an experienced machining manufacturer to adjust the bath solution to reduce the risk of color discrepancies. However, the cost will naturally be higher due to yield rate control.
6061 aluminum is the clear and reliable choice for component designs requiring welding operations. It exhibits excellent weldability using techniques such as the common TIG or MIG, maintaining structural integrity across joined assemblies. Conversely, 7075 aluminum is not recommended for welding needs. This is because its high zinc and copper content will make the 7075 suffer liquid metal embrittlement and solidification segregation during welding, which almost inevitably leads to internal micro-cracking and joint failure under stress.
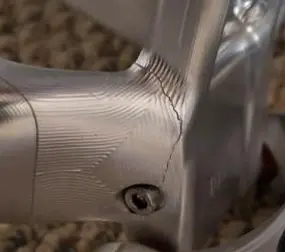
In projects demanding the extreme strength of 7075, welding must be strictly avoided to prevent critical safety hazards. Instead, assemblies specifying 7075 should rely on alternative non-welding joining techniques, such as mechanical fasteners and dowel pins, structural adhesive bonding, interference/press fits, or interlocking joint designs.
The main alloying elements of 6061 aluminum alloy are magnesium (Mg) and silicon (Si), with an extremely low copper (Cu) content. In typical indoor or dry environments, 6061 aluminum alloy inherently possesses quite good rust and corrosion resistance, offering noticeably better baseline corrosion resistance compared to 7075.
However, it is relatively rare to see 6061 aluminum used without any surface protection. Unless the part is used strictly in a dry indoor environment, has no aesthetic requirements, or serves as an internal structural component under extremely tight budget constraints, you can skip surface finishing for 6061 aluminum parts. In most engineering applications, however, surface treatment is still recommended to enhance 6061 durability (most commonly: Type II anodizing for cosmetic color, and Type III hardcoat anodizing for scratch resistance, both of which improve corrosion resistance).
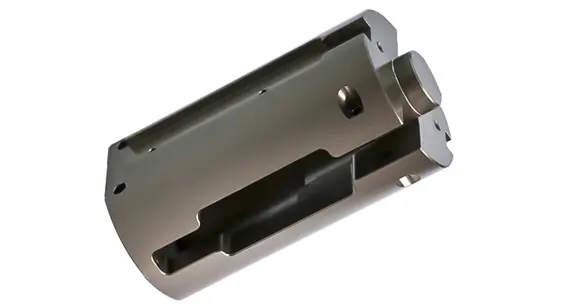
By contrast, 7075 aluminum alloy has poorer natural corrosion resistance due to its higher proportions of zinc and copper, particularly because copper tends to form micro-galvanic cells within the microstructure, leading to localized electrochemical corrosion. As mentioned earlier, 7075 is less suitable than 6061 for Type II anodizing and high-aesthetic applications. Therefore, you can choose Type III hardcoat anodizing, powder coating, or anti-corrosion coatings to protect 7075 aluminum components from corrosion (especially stress corrosion cracking).
(Based on a medium-sized, simple-geometry component batch of 500 units)
| Material | Surface Finishing Option | Additional Cost Increase (%) | Additional Lead Time | Key Drivers and Risk Factors |
| 6061-T6 | Type II Anodizing (Cosmetic / Vivid Colors) | Baseline (+10% – 15%) | +2 – 3 Days | Excellent process yield, highly predictable color consistency, minimal bath management required. |
| 6061-T6 | Type III Hardcoat Anodizing | +20% – 30% | +3 – 4 Days | Standard hardcoat processing; produces a thick, wear-resistant oxide layer. |
| 6061-T6 | Chromate Conversion / Chem Film (Passivation) | +8% – 12% | +1 – 2 Days | Economical anti-corrosion barrier with low thickness impact; excellent conductive surface base. |
| 6061-T6 | Electropolishing / Chemical Polishing | +15% – 25% | +2 – 3 Days | Removes microscopic burrs and smooths surface features to improve corrosion barrier performance. |
| 6061-T6 | Bead Blasting + Type II Anodizing | +18% – 25% | +3 – 4 Days | Mechanical blasting removes machining lines prior to anodizing for a uniform matte finish. |
| 7075-T6 / T651 | Type II Anodizing (Cosmetic / Vivid Colors) | +25% – 40% | +4 – 6 Days | High rework/scrap risk due to copper-induced yellow/gray tinting; requires custom bath tuning and strict QA. |
| 7075-T6 / T651 | Type III Hardcoat Anodizing | +25% – 35% | +3 – 5 Days | Recommended primary protective finish for 7075; slightly higher bath monitoring needed vs. 6061. |
| 7075-T6 / T651 | Chromate Conversion / Chem Film (Passivation) | +12% – 18% | +2 – 3 Days | Provides essential corrosion prevention for tight-tolerance aerospace parts where thickness of other coatings is prohibited. |
| 7075-T6 / T651 | Low-Temp Powder Coating | +30% – 45% | +4 – 6 Days | Requires low-bake formulations (~150°C) and strict oven cycle control to avoid over-aging the alloy temper. |
| 7075-T6 / T651 | Bead Blasting + Type III Hardcoat | +30% – 40% | +4 – 5 Days | Creates a durable, non-reflective matte protective surface while hiding tool marks. |
Relatively speaking, 7075 aluminum has higher hardness, allowing it to cut crisply during machining. Chips break easily, leaving minimal, tiny edge burrs that can be brushed off with ease. In contrast, 6061 aluminum is relatively softer and more ductile. During high-speed milling (roughing) or drilling operations, it is prone to forming gummy, elongated burrs along exit edges and thin-walled features. However, to keep burring under control, machine shops typically adjust cutting speeds and employ sharper tooling during the finishing stage.
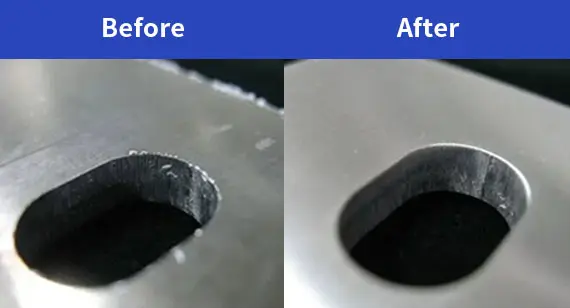
The volume of burrs directly impacts post-processing labor costs and lead times. When it comes to post-machining deburring steps, such as vibratory tumbling, chemical polishing, or bead blasting, 6061 does not offer the same cost and time advantages as 7075. This can be kind of an advantage of 7075 aluminum.
Both 6061 and 7075 carry a risk of warping and dimensional distortion when machining thin-walled structures. However, because 7075 has higher material strength and significantly greater internal residual stress, its risk of machining deformation is noticeably higher than that of 6061.
Generally speaking, pre-stretched aluminum in the T651 temper offers superior dimensional stability over the T6 temper for thin-walled parts, as the pre-stretching process relieves the vast majority of internal residual stress.
Even so, 6061-T6 remains the far more common and cost-effective choice for general structural designs and everyday applications, even for many industrial thin-walled or precision components, since its residual stress is manageable without upgrading to T651. Higher-cost 6061-T651 is usually less used and reserved for extreme high-precision scenarios with strict tolerances, such as aerospace parts or precision optics.
Conversely, 7075 aluminum is inherently a premium material designed for high-performance applications (it is called aerospace aluminum). Given its high cost-baseline and severe residual stress, pairing it with the T651 temper (7075-T651) becomes the far more standard choice for thin-walled and precision components.
With its excellent balance of weldability, corrosion resistance, and cost-efficiency, 6061 aluminum serves as the industry standard for a wide range of structural, functional, and decorative components across automotive manufacturing, building construction, industrial automation, and consumer electronics. In contrast, 7075 aluminum is chosen specifically when maximum strength and performance take priority over cost and joining ease; its exceptional strength-to-weight ratio makes it indispensable for high-load precision applications in aerospace airframes, defense hardware, missile structures, and high-performance sports equipment like racing bicycle frames.
6061 CNC Machined Part Examples:
7075 CNC Machined Part Examples:
How We Advise Automotive Client on Material Selection for Suspension Rockers and Achieve Precision, Zero Distortion, Wear-Resistant Surfaces, and a ±0.03mm Hole Pitch Tolerance.
An automotive client required a batch of lightweight, high-load suspension rocker arms. The part featured thin structural ribs and two critical pivot bores requiring a tight hole-to-hole center distance tolerance of ±0.03mm. Initially, the client's design drawing specified 7075-T6 material, citing peak dynamic load requirements.
However, out of concern for potential machining distortion during CNC processing and yield control under strict tolerances, our machine shop engineers initiated further communication with the client. We found that although the part operates under high-stress conditions, structural stress simulations confirmed that 7075-T651 fully meets the load requirements. Given that 7075-T6 contains high internal residual stress , metal removal during rough milling and finishing passes posed a risk of stress-induced thin-wall warping and bore pitch deviation. Therefore, we recommended upgrading the material specification to pre-stretched stress-relieved 7075-T651 aluminum. The client finally decided to use 7075-T651 aluminum for their suspension rocker arms.
During the machining process, we implemented a symmetrical layered roughing routine with intermediate stress-relief pauses to remove much of the residual stresses. Additionally, for the thin-walled sections and pivot bores, the finishing stage utilized specialized vacuum fixtures and soft-jaw low-clamping-force workholding, paired with high-spindle-speed, light-depth-of-cut milling passes to prevent micro-deformations caused by clamping force or cutting heat. For surface protection, to withstand harsh outdoor wear and corrosive environment demands, we applied a Type III Hardcoat Anodizing process, pre-calculating a 20–25 µm oxide film thickness compensation during design to ensure surface hardness reached 400+ HV without compromising bore dimensional accuracy.
Ultimately, the production batch achieved an exceptional 99.8% yield rate, with the aluminum suspension rockers maintaining zero post-fixture distortion and consistently holding the critical ±0.03mm hole distance tolerance. Furthermore, precise dimensional control and the hardcoat anodized finish allowed the parts to seamlessly pass the client's rigorous dynamic fatigue and corrosion testing without secondary straightening or grinding operations, reducing overall manufacturing and inspection costs by approximately 15%.
This guide has systematically explored the core differences between 6061 and 7075 aluminum alloys for CNC machining, covering mechanical properties, processability, surface treatment characteristics, and engineering trade-offs. By understanding how 6061 excels in weldability, cosmetic anodizing, and cost efficiency, while 7075 dominates high-load, high-performance applications, you can make more informed material selection decisions for your specific project requirements. Furthermore, accounting for post-processing factors, such as temper selection (e.g., T6 vs. T651), burr formation, thin-wall distortion, and corrosion protection, ensures that your parts meet strict functional and aesthetic standards without incurring unexpected lead-time or budget overruns. Have a challenging 6061 or 7075 aluminum component drawing ready for review? Contact our engineering team to discuss material selection, temper options, DFM recommendations, and custom surface finishing strategies tailored to your application. [2D Drawings (PDF files), 3D Drawings (IGS/STP/STEP files)].
Send your 2D drawings, 3D CAD models, alloy and temper requirements, critical tolerances, wall thickness, surface-finish requirements, prototype quantity and production quantity. VMT will review material selection, DFM, machining strategy, anodizing or coating options, inspection and quotation requirements.
All information and uploaded files are secure and confidential.
1 Tell us what you need
2 Get solution & quote
3 Approve production
Email: inquiry@vimetal.com.cn
What are the main advantages of 6061 aluminum over 7075 for CNC machined parts?
6061 offers superior weldability, easier anodizing color consistency, better raw corrosion resistance, and significantly lower material and machining costs.
What are the limitations of using 7075 aluminum for CNC machined parts?
7075 cannot be welded, is prone to stress corrosion cracking without proper coatings, exhibits higher residual stress (distortion risk in thin walls), and is substantially more expensive.
Can powder coating solve color variance issues on 7075 aluminum, and what are the trade-offs?
Yes, powder coating covers 7075's copper-induced anodizing discolorations with a uniform color layer; however, the thicker coating is unsuitable for high-precision tolerances, and high curing temperatures risk degrading the alloy temper unless low-bake powders (~150°C) are used.
Which is tougher between 7075-T6 and 6061-T6, and where are they applied?
7075-T6 is significantly tougher and stronger, offering exceptional resistance to high impact, fatigue, and heavy mechanical stress, making it ideal for critical load-bearing parts like aerospace spars and racing suspension arms. In contrast, 6061-T6 provides adequate toughness for moderate loads, serving well in general structural brackets, frames, and everyday industrial housings.
What are the essential DFM tips for 6061 vs. 7075 aluminum?
Specify 7075-T651 over T6 to minimize thin-wall warping from residual stress, use low-temperature cure powder coating or Type III hardcoat for 7075 corrosion protection, and avoid welded assemblies when specifying 7075. For 6061, there are no strict or specialized DFM restrictions since it is the industry-standard general-purpose aluminum; standard design guidelines for wall thickness, tight tolerances, and internal corner radii apply, and your CNC manufacturer can provide tailored feedback based on your part drawing to optimize cycle times and costs.
Is 7075 better than 6061 for high-performance applications like racing cars and FPV drones?
Yes, 7075 is superior for high-performance components subjected to intense impact, fatigue, and structural loads, whereas 6061 remains preferable for non-critical drone arms or frames where field weldability and lower replacement costs are prioritized.
The technical information and manufacturing advice shared on the VMT website are for general guidance only. While we strive for accuracy, VMT does not guarantee that the processes, tolerances, or material properties mentioned are applicable to every specific project. Any reliance you place on such information is strictly at your own risk. It is the buyer's responsibility to provide definitive engineering specifications for any production orders. Final specifications and service terms shall be subject to the formal contract or quotation confirmed by both parties.


 +86 15099911516



 Read more