16 years one-stop China custom CNC machining parts factory
Hey there I’m VMT Sam!
With 25 years of CNC machining experience we are committed to helping clients overcome 10000 complex part-processing challenges all to contribute to a better life through intelligent manufacturing. Contact us now
 582 |
Published by VMT at Nov 07 2026 | Reading Time:About 8 minutes


While commodity aluminum prices (LME) typically fluctuate between $2.30 and $2.70/kg( last ten years, but now in 2026 it’s been $2.90 ~ $3.40 /kg affected by the energy), raw material costs are only one part of the final CNC machining quote. In general, aluminum material procurement accounts for approximately 20%–45% of the total quoted price, while the remaining 55%–80% comes primarily from CNC machining time, tooling and fixtures, workholding and setup, and surface finishing.
Therefore, rising aluminum prices do increase manufacturing costs, but their actual impact on the final part price also depends on part geometry, material utilization, machining complexity, and finishing requirements.
Quick Cost-Saving Strategies:
When aluminum prices rise, you should look beyond simply negotiating lower raw material prices. A more effective approach is to optimize the entire manufacturing process:
Case Study Overview
The end part shares a 500-unit automotive sensor housing project achieved a 21% cost reduction and 5-day shorter lead time through material substitution, DFM optimization, and near-net-shape aluminum blanks.
When purchasing CNC-machined aluminum alloy parts, you need to understand one key point: market aluminum prices, finished part weight, and order quantity do not determine the final quotation. The same part drawing can result in significantly different costs depending on the material selection, raw material dimensions, and purchase volume. Let’s look at four common scenarios:
1. Why Doesn't the Quotation for CNC Parts Decrease Significantly When Market Aluminum Prices Fall?
When LME aluminum prices or market aluminum prices fall, you could expect the quotations for CNC-machined aluminum parts to decrease accordingly. However, in actual quotation requests, suppliers’ prices for precision CNC parts often remain close to the previous quotation.
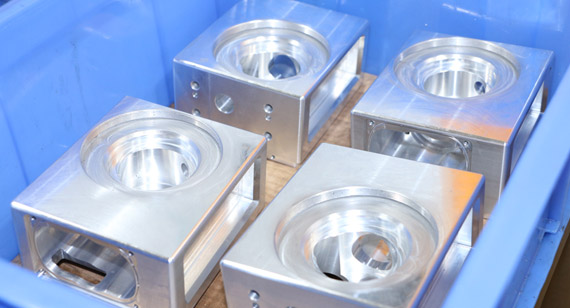
For example, in the quotation for precision camera aluminum housings , raw material accounts for 30% of the total cost, while the remaining 70% comes from machining time, fixtures and setups, quality inspection, and surface finishing. If the aluminum purchase price decreases by 5% while other manufacturing costs remain unchanged, the reduction in the final quotation will usually be relatively small.
This is not only because raw material costs account for just less portion of the final CNC machining quotation, but also because of the following factors:
Therefore, to assess the actual impact of aluminum price changes on part quotations, you need to consider both the proportion of raw material costs and the costs of other manufacturing processes, rather than looking only at the rise and fall of LME aluminum prices.
2. Why Do Parts of the Same Size Have Such Different Quotations When Different Aluminum Alloy Grades Are Used?
(Taking the two most popular aluminum alloys, 6061 and 7075, as examples.)
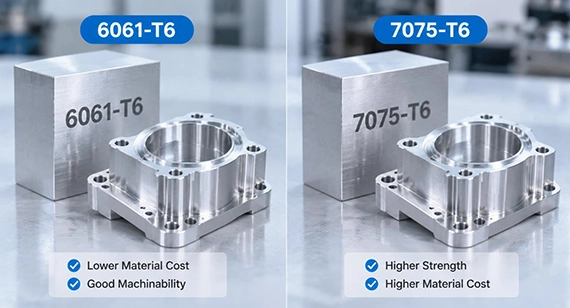
For CNC machiend aluminum parts with basically the same dimensions, structure, and machining requirements, simply changing the material from 6061-T6 to 7075-T6 can result in a significant difference in the final quotation, with the total price potentially increasing by nearly 50%.
3. Why Is the Raw Material Cost Calculated Based on 1 kg When the Finished Part Weighs Only 200 g?
This is another common concern.
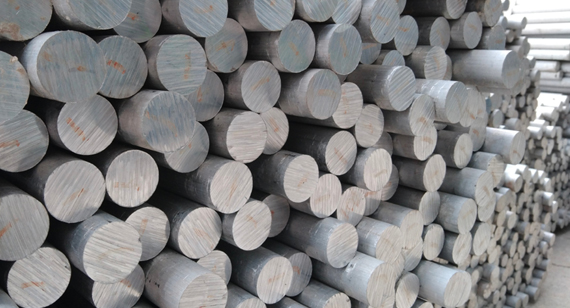
This is because CNC milling or turning requires removing excess material from larger aluminum plates, square bars, or profiles, rather than purchasing raw material based on the finished part weight.
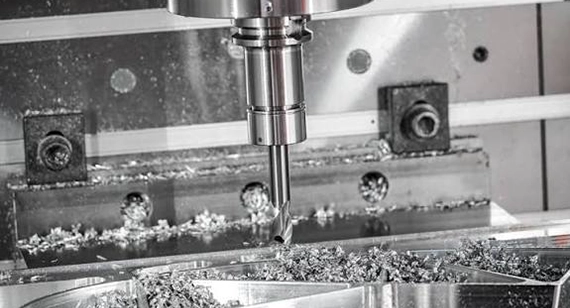
The main reasons include:
4. Why Is the Per-Part Aluminum Material Cost So Different Between Small-Batch Prototypes and Mass Production of Thousands of Parts?
For parts made from the same drawing and aluminum alloy grade, the material cost per part differs significantly between small-batch vs large-volume orders. The main factors include:
For long-term purchasing projects, provide your estimated annual demand in advance so that the supplier can evaluate centralized material purchasing, production in batches, and phased deliveries to reduce the costs of your CNC-machined aluminum parts project.
Since the price of CNC-machined aluminum parts is not determined by aluminum material costs alone, you need to take a comprehensive approach to material selection, CAD structural design, and purchasing plans. Optimize part manufacturability in advance to reduce unnecessary costs while meeting functional requirements.
1. Choose the Right Aluminum Alloy Grade and Avoid Unnecessary High-Performance Materials (e.g., 6061 vs. 7075)
Not all CNC aluminum alloy parts need high-strength materials such as 7075-T6. For general structural brackets, equipment housings, and mounting components, if there are no special requirements for high strength, fatigue resistance, or load-bearing capacity, first evaluate whether 6061-T6 meets the design requirements.
6061-T6 offers good overall mechanical properties, corrosion resistance, and machinability, while 7075-T6 is more suitable for applications with higher strength and strength-to-weight ratio requirements. Selecting the appropriate aluminum alloy grade based on the actual load, operating environment, and mechanical requirements of the part controls raw material costs and some machining costs associated with the material grade.
2. Optimize Internal Corner Radii to Match Standard End Mill Sizes
For CNC aluminum alloy parts with cavities, grooves, and complex contours, excessively small internal corner radii require smaller-diameter end mills. This increases machining time and tool wear. In some cases, additional corner-cleaning operations are also required, increasing costs.
Therefore, without affecting assembly and functionality, consider appropriately increasing internal corner radii, for example, using R3 or R5 radii that match standard cutting tools more easily. This reduces the need for special small-diameter tools, optimizes tool paths, and reduces unnecessary machining time and costs.
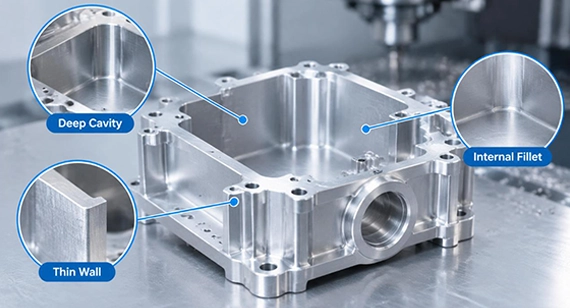
3. Reasonably Control Aspect Ratios and Wall Thickness to Reduce Thin-Wall Machining Risks
For parts such as robot joint housings, lightweight brackets, and precision equipment housings, excessively deep cavities and thin walls increase machining difficulty.
This is because deep cavities require long-reach cutting tools, reducing tool rigidity. Thin-wall structures are prone to vibration and elastic deformation under cutting forces, affecting final dimensional accuracy.
In this situation, the higher rigidity of 7075 gives it an advantage over 6061, 5052, and 6063, even though its material cost is indeed higher.
Recommended Wall Thickness and Cavity Depth Values for Different Aluminum Alloy Grades
| Aluminum Series & Grade | Absolute Limit Wall Thickness | Recommended Safe Wall Thickness | Recommended Cavity Depth-to-Tool Diameter Ratio (Aspect Ratio / L) | Typical Cutting Characteristics and Design Recommendations |
| 6xxx series (e.g., 6061-T6) Medium-to-high strength, general-purpose | 0.5 mm | 0.8 mm | ≤ 4:1 (maximum 6:1) | Good machinability and balanced rigidity: One of the most common aluminum grades on the market. Thin walls are highly susceptible to tool vibration and thermal deformation. Follow the 4:1 stability guideline. |
| 7xxx series (e.g., 7075-T6) Ultra-high strength, aerospace-grade | 0.4 mm | 0.6–0.8 mm | ≤ 6:1 (maximum 8:1) | Excellent rigidity, high internal stress: Its high hardness provides good resistance to tool deflection. It supports thinner walls without easily collapsing. However, internal stress is extremely high, and large-area cavity machining easily causes overall warping. A finishing allowance must be reserved. |
| 2xxx series (e.g., 2024 / 2017) High hardness, aluminum-copper alloys | 0.5 mm | 0.8 mm | ≤ 5:1 (maximum 6:1) | Good chip formation and high toughness: High fatigue strength and good machinability, but poor corrosion resistance. Thin-wall edges are prone to small tears caused by cutting heat or localized brittleness. |
| 5xxx / 3xxx series / pure aluminum (e.g., 5052, 1060) | 1.0 mm | 1.5–2.0 mm | ≤ 2:1 (deep cavities not recommended) | Soft and sticky material, highly prone to deformation: Soft aluminum or non-heat-treatable corrosion-resistant aluminum easily sticks to the cutting tool and produces continuous ribbon-like chips. Thin-wall and deep-cavity designs must be strictly avoided, otherwise severe deformation and surface damage occur during machining. |
4. Ask the Machining Factory to Consolidate Purchasing Batches and Reduce Material Costs Through Bulk Material Preparation
When your team needs to purchase the same CNC aluminum alloy parts over the long term, provide the supplier with your estimated annual demand in advance, rather than only the purchase quantity for the current batch. Informing the CNC machining factory of your estimated annual purchasing volume allows the supplier to purchase the required raw materials in larger quantities when aluminum prices are relatively low, then machine and deliver the parts in batches according to actual production requirements. The resulting material cost savings are ultimately reflected in more favorable quotations.
Through early-stage engineering reviews, machining process optimization, and supply chain management, the CNC machining factory can help the project reduce the cost impact of raw material price fluctuations, material waste, and improve machining efficiency.
Method 1: Provide Free Preliminary DFM (Design for Manufacturability) Reviews
Before production, they conduct a manufacturability review of the 3D CAD drawings provided by clients.
Method 2: Optimize Material Nesting and Multi-Axis Machining
They will use CAD/CAM software to optimize the nesting layout of multiple parts on the same piece of raw material.
Method 3: Establish a Stable Raw Material Supply Chain and Inventory Management System
Build long-term partnerships with reliable aluminum suppliers and maintain reasonable inventory levels of commonly used aluminum alloys, such as 6061, 7075, and 5052.
Method 4: Optimize Cutting Strategies and Machining Processes to Improve Efficiency
Select appropriate cutting tools and machining parameters based on the characteristics of aluminum alloys and the geometry of each part.
A European automotive industry client approached us with an urgent demand for 500 units of custom CNC-machined aluminum sensor housings. The component was designed to protect precision internal electronics in demanding under-the-hood environments. With tight delivery deadlines and strict mechanical reliability requirements, the client needed a manufacturing partner capable of meeting high tolerance standards while balancing tight project development budgets.
During our initial technical review, several critical cost drivers emerged. The original engineering drawing specified aerospace-grade 7075-T6 aluminum, featured a deep 45 mm cavity, and maintained an ultra-thin 0.8 mm internal wall thickness. Furthermore, global raw aluminum prices had increased during this procurement window. The combination of increased raw stock price, high risk of tool chatter and deflection in the deep cavity, and lower feed rates pushed the initial machining quote roughly 40% over the client’s target budget.
Engineering Optimization & DFM Collaboration
Rather than rejecting the budget, our engineering team conducted a detailed Design for Manufacturability (DFM) review and proposed a three-step optimization strategy:
Material Downgrading: Finite element and operating condition evaluations confirmed the housing was a non-load-bearing protective enclosure. We recommended switching from 7075-T6 to standard 6061-T6, cutting raw material procurement cost by approximately 30% without compromising environmental or structural integrity.
Feature & Toolpath Optimization: We collaborated with the client's design team to relax the wall thickness to 1.5 mm and increase the internal corner radii to R4. This reduces chatter vibration in the deep cavity, allowed larger standard end mills, and boosted milling feed rates by 35%.
Near-Net-Shape Blanks: Instead of machining down from standard solid aluminum billets (which wasted 78% of the metal), we sourced custom-extruded aluminum profile stock closely matching the external envelope, ruducing the material removal rate down to just 38%.
Results & Ongoing Partnership
Through these targeted design and process enhancements, our engineering team successfully brought the final per-part quote down by 21%, directly resolving the client’s budget crisis while reducing production lead time by 5 days. The initial prototype batch passed rigorous dimensional inspection and environmental sealing tests on the first try. Impressed by our engineering transparency and cost-saving capabilities, the project was transitioned into recurring quarterly batch orders.
Bulk aluminum prices are influenced by global market supply and demand, as well as raw material market conditions. However, the final machining cost of an individual CNC part is not determined by aluminum prices alone. Other factors that directly affect the final quotation include material utilization, machining difficulty caused by part geometry, and the time and material losses involved in the manufacturing process. For long-term purchasing projects, choosing a CNC machining factory that can evaluate material costs, machining efficiency, and supply chain resources together is often more beneficial for controlling overall procurement costs than simply comparing aluminum prices per kilogram.Through appropriate material selection, structural design, raw material blank optimization, and machining process planning, as well as good communication and cooperation with your CNC machining factory and the adoption of cost-optimization DFM recommendations, your team can proactively control some of the otherwise unnecessary costs.
Planning a new aluminum CNC machining project or facing a quotation that exceeds your budget? Send your drawings to our engineering team for a free DFM review, cost optimization recommendations, and a quotation within 24 hours. [ We support 2D Drawings (PDF files), 3D Drawings (IGS/STP/STEP files)].
Send your 2D drawings, 3D CAD models, aluminum grade, tolerance requirements, surface finish, prototype quantity, production quantity and annual demand. VMT will review material selection, blank dimensions, material utilization, DFM, machining strategy, surface finishing and cost optimization before quotation.
All information and uploaded files are secure and confidential.
1 Tell us what you need
2 Get solution & quote
3 Approve production
Email: inquiry@vimetal.com.cn
Q1: What percentage of CNC machining cost comes from aluminum raw material?
A: Typically, raw material accounts for 20% to 45% of the total cost for aluminum CNC parts. For simple geometry with low material removal, it can be higher; for complex thin-walled parts requiring hours of 5-axis milling, machining labor and machine time dominate over 70% of the cost.
Q2: Why is 7075 aluminum machining significantly more expensive than 6061?
A: First, 7075 raw stock costs roughly 50%–80% more per kilogram than 6061 due to its high zinc and magnesium alloy content. Second, its material properties can affect cutting parameters, tool selection, and machining time, increasing overall production costs.
Q3: How does the chip rate affect my final aluminum part price?
A: CNC is a subtractive manufacturing process. For a part that removes 80% of an aluminum billet, the buyer should pay for the full starting block plus the machining time required to mill away that material.
Q4: Can raw aluminum price fluctuations change my quote after an order is placed?
A: At VMT CNC Machining Factory, once an official quotation is confirmed and the order is locked within its validity period (typically 15–30 days), we are responsible short-term raw material fluctuations. For annual recurring orders, price adjustments are pegged transparently to agreed quarterly prices.
Q5: How do I get an accurate cost estimate for my custom aluminum machining project?
A: Provide complete 3D CAD files , detailed 2D drawings with tolerances and surface finish specifications, your target alloy grade (e.g., 6061-T6), and batch quantities. Our engineering team will review the geometry for material optimization and issue a detailed quotation.
Q6: Which aluminum grade offers the best balance of price and performance for prototypes?
A: 6061-T6 is the best-fit for prototyping and general production. It offers a competitive cost per kg among structural alloys, exhibits outstanding machinability, is readily available in common stock sizes, and accepts anodizing exceptionally well.
The technical information and manufacturing advice shared on the VMT website are for general guidance only. While we strive for accuracy, VMT does not guarantee that the processes, tolerances, or material properties mentioned are applicable to every specific project. Any reliance you place on such information is strictly at your own risk. It is the buyer's responsibility to provide definitive engineering specifications for any production orders. Final specifications and service terms shall be subject to the formal contract or quotation confirmed by both parties.


 +86 15099911516



 Read more