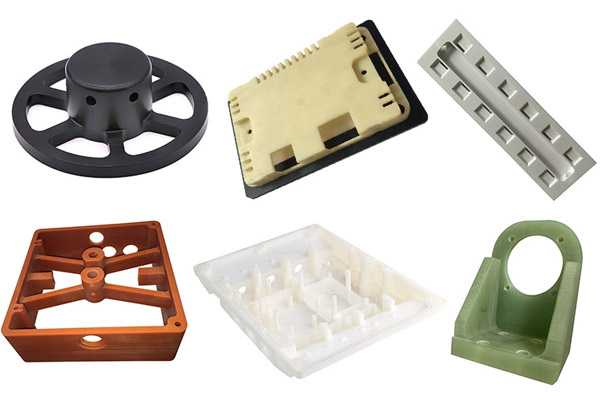
16 years one-stop China custom CNC machining parts factory
Hey there I’m VMT Sam!
With 25 years of CNC machining experience we are committed to helping clients overcome 10000 complex part-processing challenges all to contribute to a better life through intelligent manufacturing. Contact us now
 823 |
Published by VMT at Oct 09 2026 | Reading Time:About 6 minutes


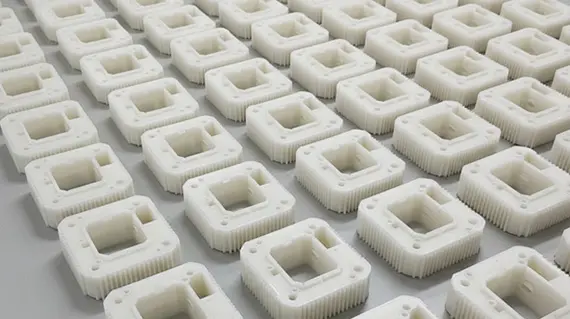
Nylon is a vital engineering plastic and synthetic fiber that has played a pivotal role across numerous industries since its inception. It is widely used to replace lower-strength metal components in automotive engines, as well as serve as an excellent option for electrical insulation, industrial wear resistance, and self-lubricating parts.
However, with a vast range of nylon grades available (such as PA6, PA66, and PA12), choosing the wrong material can lead to critical issues like dimensional instability caused by moisture absorption or thermal deformation under high temperatures. Furthermore, nylon manufacturing encompasses various processes, including CNC machining, 3D printing, injection molding, and extrusion. Determining which process aligns best with your chosen grade in terms of cost, volume, precision, and surface roughness is essential to maximizing both product quality and cost-efficiency.
Overview
This article provides a comprehensive overview of nylon properties, types, characteristics, limitations, and applications. It also explores grade and process selection strategies, common manufacturing challenges in CNC machining nylon parts, and how our factory resolves them to support your product development team. Finally, we also share a case study: how we advised an automotive client facing material cost pressures to replace aluminum 6061 with PA66 + 30% GF for an intake manifold with a relatively simple internal cavity. By utilizing rapid injection molding paired with secondary CNC machining for a 2,000-unit run, we helped them achieve a 50% weight reduction and a 28% cost savings, all while delivering superior vibration and fatigue resistance.
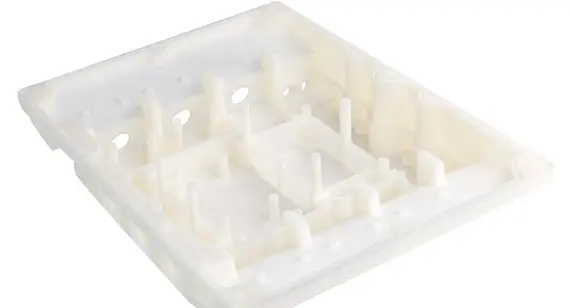
Nylon, also known as polyamide (PA), was the world’s first fully synthetic fiber, developed by American chemist Wallace Carothers and his team at DuPont. As a versatile thermoplastic resin, nylon is defined by repeating amide groups (-NHCO-) along its molecular backbone, giving the material exceptional mechanical strength, heat resistance, wear resistance, and chemical stability.
Excellent Characteristics of Nylon (The Advantages)
1. Exceptional Mechanical Performance
2. Thermal Stability
3. Tribological and Surface Properties
4. Chemical and Environmental Resistance
5. Physical and Electrical Capabilities
To select the right polyamide for your engineering application, it is essential to compare key mechanical, thermal, and physical properties across different standard and reinforced grades.
Comparison Table of Nylon Grades Properties
The table below provides typical values for neat (unfilled) and glass-fiber reinforced nylon resin grades:
| Property | PA6 | PA66 | PA11 | PA12 | PA66 + 30% GF |
| Melting Point (°C) | 220 | 260 | 185 | 178 | 260 |
| Typical Injection Temp (°C) | 230- 280 | 270- 300 | 210- 260 | 200- 250 | 280- 310 |
| HDT @ 1.8 MPa (°C) | 60- 70 | 75- 90 | 45- 55 | 50- 60 | 240- 250 |
| Tensile Strength (MPa) | 75- 85 | 80- 90 | 45- 55 | 45- 50 | 165- 180 |
| Flexural Strength/ Modulus (MPa) | 110/ 2,800 | 120/ 3,000 | 60/ 1,400 | 65/ 1,500 | 250/ 8,500 |
| Specific Gravity (g/cm³) | 1.13 | 1.14 | 1.04 | 1.02 | 1.37 |
| Mold Shrinkage (%) | 1.0- 1.5 | 1.2- 2.0 | 1.0- 1.8 | 0.8- 1.5 | 0.3- 0.8 |
| Water Absorption (24h/ Saturation %) | 1.8/ 9.5 | 1.3/ 8.5 | 0.2/ 1.9 | 0.1/ 1.5 | 0.7/ 5.5 |
Which Nylon Material Suits Your Project?
Instead of evaluating materials purely by their chemistry, match the grade to your specific engineering requirements and environmental constraints.
1. High Cost-Efficiency and Balanced Mechanical Strength
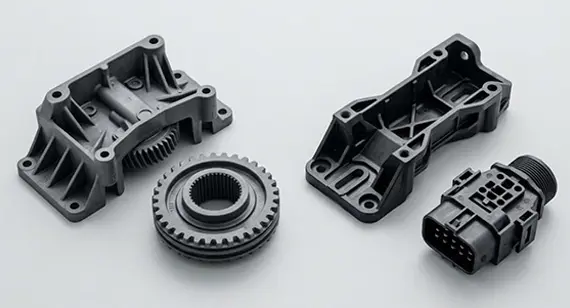
2. High Dimensional Stability, Low Moisture Absorption, and Low-Temperature Toughness
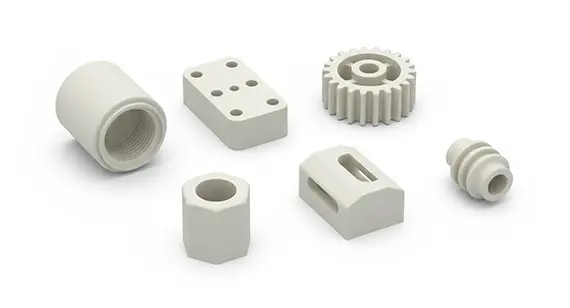
3.Good Rigidity, Load-Bearing Capacity, and Metal Replacement
4. Special Niche Polyamides (PA610 and PA1010)
5.Material Resin Cost Comparison
When evaluating project feasibility, raw material cost is a primary decision factor across different polyamide grades:
While nylon is one of the most versatile engineering thermoplastics, untreated base grades possess inherent physical and chemical limitations:
1. Moisture Absorption and Dimensional Sensitivity
2. Vulnerability to Strong Acids and Oxidizing Agents
3. High Thermal Expansion Coefficient
4. Susceptibility to Ultraviolet (UV) Degradation
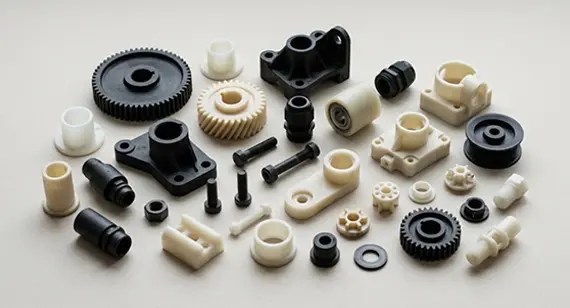
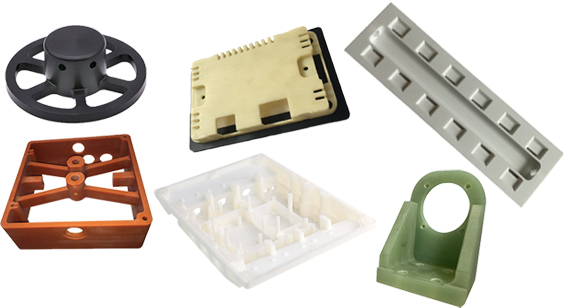
Nylon materials are widely used in machinery, automotive, electrical, textile equipment, chemical equipment, aerospace, and metallurgy. Here are a few of the examples:
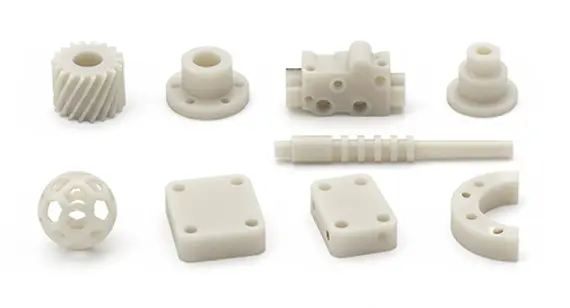
In CNC machining or 3D printing, nylon materials are often used to manufacture various low-volume parts and prototype development. These parts can also be produced by continuous extrusion for high volume profiles, and injection molding for mass cost-effective production.
CNC Machining
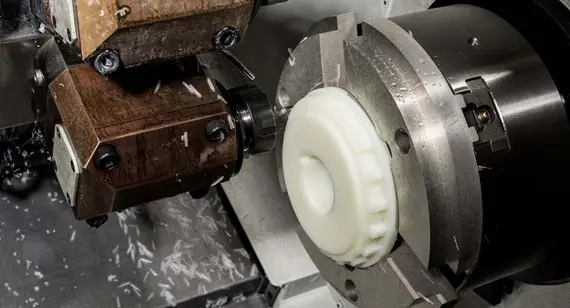
CNC machining is a high-precision, high-efficiency processing method suitable for manufacturing nylon parts with various complex shapes. CNC machining can precisely control the dimensions(about ±0.02 mm) and shapes of the parts, ensuring accuracy and quality.
3D Printing
3D printing technology can quickly transform digital models into physical parts, particularly suitable for prototype development and rapid manufacturing. Using nylon materials for 3D printing can produce high-precisions(about ±0.03mm), high-performance nylon parts.
Injection Molding
Injection molding is a method for mass-producing nylon parts. By heating the nylon material to a molten state and injecting it into a mold, then cooling and solidifying it, the desired parts are obtained. Injection molding can manufacture complex-shaped, dimensionally accurate nylon parts. Rapid injection molding has the differences of it only uses rapid mold made by aluminum or soft steel which less durible than harden steel of that of injection molding.
Extrusion Molding
Extrusion molding is rocess where heated nylon resin is forced through a shaped die to create continuous profiles. It has the advantages of high production efficiency and low per-meter costs for uniform cross-sectional geometries.
Comparison Table of Process Matching
To help your team select the right process, the following table compares key manufacturing capabilities:
| Feature | 3D Printing | CNC Machining | Rapid Injection Molding | Injection Molding | Extrusion Molding |
| Primary Goal | Rapid prototyping and visual validation | High-precision custom parts and low-volume orders | Bridge production and market testing | High-volume mass production | Continuous long profiles, tubes, and bars |
| Dimensional Precision | ±0.30 mm | ±0.02 mm | ±0.08 mm to ±0.15 mm | ±0.05 mm to ±0.12 mm | ±0.15 mm to ±0.50 mm |
| Surface Roughness (Ra) | 6.3 μm to 12.5 μm | 0.8 μm to 3.2 μm | 0.8 μm to 1.6 μm | 0.4 μm to 1.6 μm | 1.6 μm to 6.3 μm |
| Geometric Complexity | High (Internal cavities, undercuts) | Moderate to high (Prismatic geometries) | Moderate to complex (Requires mold draft angles) | High complexity (Automated side-actions and slides) | Constant cross-section only (Tubes, bars) |
| Optimal Quantity | 1 – 50 pieces | 1 – 500 pieces | 1,000 – 5,000 pieces | 10,000+ pieces | Continuous / High volume |
| Recommended Nylon Grades | PA12, PA11 (SLS powder) | Extruded PA6, PA66, PA12 stock bars/plates | Injection grade PA6, PA66, PA66 + 30% GF | Injection grade PA6, PA66, PA66 + 30% GF | Extrusion grade PA6, PA12, PA610 |
| Unit Cost | Higher per-part cost | Moderate per-part cost; cost driven by machining time | Moderate aluminum/soft steel mold cost; low to moderate per-part unit cost | High hardened steel mold cost; lowest per-part unit cost(amortize the tooling cost over a high-volume production run) | Low cost per linear meter |
For complex nylon components requiring both low unit cost and ultra-tight critical tolerances (such as ISO IT6 precision bearing seats, seal grooves, or fine internal threads), a hybrid production approach is recommended. Parts are first net-shaped via rapid or production injection molding, followed by targeted secondary CNC machining on critical features. This combined process maximizes production speed while guaranteeing micro-inch dimensional accuracy.
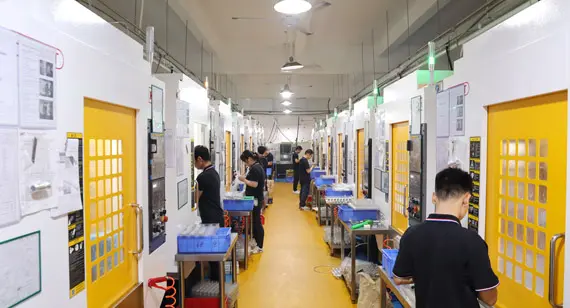
In practical engineering applications, CNC machined nylon parts may encounter common challenges such as dimensional changes, warping deformation, stress cracking, wear acceleration, and static accumulation. Resolving these issues requires aligning your part design with specialized manufacturing best practices:
Dimensional Changes
Nylon materials exhibit high water absorption, which can cause volumetric expansion and dimensional changes during machining and service. To prevent this, a professional CNC machining factory typically pre-dries raw nylon stock in temperature-controlled ovens and maintains strict ambient humidity control across the shop floor. On the design side, you can also specify low-water-absorption grades such as PA12 or PA11 for components requiring tight tolerances.
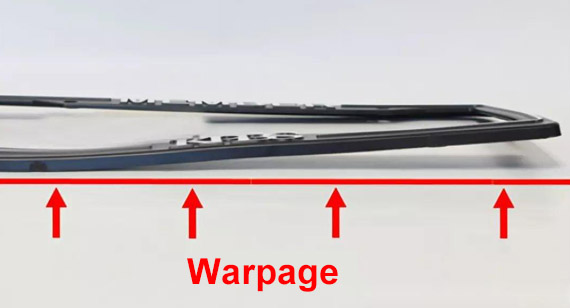
Deformation and Warping
Nylon stock often deforms due to the uneven release of internal residual stress during heavy material removal. Experienced manufacturing partners usually subject raw stock to a stress-relief annealing heat treatment prior to cutting, utilizing sharp carbide tools with optimized feed rates. Meanwhile, you may consider these design tips of designing uniform wall thicknesses and specifying balanced material removal across symmetrical surfaces.
Cracking
Nylon parts can experience surface micro-cracking due to localized heat concentration and geometric stress points. The parts design should avoid sharp 90-degree internal corners by specifying generous radii (such as R 1.5 mm or larger) to distribute mechanical loads. During production, qualified suppliers will employ razor-sharp, high-rake cutting tools and adequate air cooling to control cutting temperatures and prevent thermal stress cracks.
Wear Resistance Decline
While nylon features good native friction properties, components under heavy continuous sliding or high-load conditions may still suffer surface wear over time. You may choose self-lubricating grades such as MoS2-filled or oil-filled nylon, or request the manufacturing partner to apply specialized wear-resistant and anti-friction coatings on mating components.
Static Issues
As an electrical insulator, nylon is prone to accumulating triboelectric static charge during high-speed machining and handling, attracting fine plastic dust. This can be solved by specifying permanent anti-static additives or conductive carbon-black fillers in the material callout, while professional machine shops will utilize ionized air blowers during machining and final cleaning to neutralize surface electrostatic charges.
Replacing Aluminum 6061 with PA66 + 30% GF to Cut Intake Manifold Costs by 28%
An automotive client approached our engineering team looking to produce an engine intake manifold with a relatively simple internal cavity. The component was originally designed to be machined from solid 6061 aluminum to withstand high under-hood temperatures and vibration. However, high raw material costs, long machining times, and new lightweight vehicle requirements prompted the team to explore a more economical, lightweight alternative that could still match metal-level performance.
After evaluating the operating thermal range and mechanical stress requirements, we recommended replacing 6061 aluminum with PA66 + 30% Glass Fiber (GF). Reinforced with 30% glass fibers, this specialized nylon grade offers exceptional tensile strength, a high heat deflection temperature (HDT up to 250°C), and excellent long-term fatigue resistance under continuous engine heat and vibration.
Since the required volume was a medium batch of 2,000 pieces, building expensive mass-production steel molds was not cost-effective. Instead, we recommended a hybrid approach: shaping the main body using rapid injection molding with lower-cost tooling, followed by secondary CNC machining only on critical mounting holes and sealing surfaces to guarantee tight tolerances.
By adopting this material and manufacturing strategy, our client achieved substantial project benefits:
In this engineering guide, we have explored the essential characteristics of nylon (polyamide) materials, detailed key engineering grades (such as PA6, PA66, PA12, and glass-reinforced PA66+30%GF), outlined practical machining solutions to prevent cracking and moisture absorption, and presented a process selection matrix covering 3D printing, CNC machining, injection molding, and extrusion. Through our automotive intake manifold case study, you can see how replacing metal with high-performance nylon and applying hybrid manufacturing techniques like rapid injection molding with secondary CNC machining can drastically reduce weight and costs while maintaining strict dimensional precision. With these material properties and process insights, I believe this guide is helpful for you to successfully optimize part designs, reduce material expenses, and accelerate production timelines for demanding applications.
Have a complex nylon component design or considering a metal-to-plastic conversion for your upcoming project cost optimization? Upload your drawings for a fast DFM analysis or get the solution of selecting the ideal nylon grade and manufacturing process for your exact specifications. [2D Drawings (PDF files), 3D Drawings (IGS/STP/STEP files)].
Send your 2D drawings, 3D CAD models, nylon grade, tolerance requirements, operating environment, prototype quantity and production quantity. VMT will review material selection, DFM, CNC machining, 3D printing, injection molding or extrusion options, inspection and quotation requirements.
All information and uploaded files are secure and confidential.
1 Tell us what you need
2 Get solution & quote
3 Approve production
Email: inquiry@vimetal.com.cn
How does Polyimide (PI) compare to Nylon in high-temperature applications?
Polyimide offers exceptional thermal stability and can withstand continuous operating temperatures above 250°C, whereas standard nylon grades begin to soften around 90°C to 120°C. While polyimide is significantly more expensive and difficult to process, it is selected over nylon when extreme thermal performance and minimal outgassing are required.
What are the key differences when choosing between Delrin (POM) and Nylon for CNC machining?
Delrin (acetal) absorbs far less moisture than nylon, giving it superior dimensional stability in wet environments and making it easier to hold micro-inch tolerances during machining. However, nylon provides higher wear resistance, superior impact strength, and better performance under heavy dynamic loads.
What are the common glass-filled nylon types and their main engineering benefits?
The most widely used variants of glass-filled nylon are PA6 + 30% GF and PA66 + 30% GF, which incorporate short glass fibers into the polyamide matrix. Adding glass filler drastically increases tensile strength, flexural modulus, and heat deflection temperature (HDT), making these grades ideal for metal replacement in structural housings.
When will you choose UHMW over Nylon for wear parts?
UHMW features a low coefficient of friction and superior chemical and moisture resistance, making it superior for chute liners, wet environment wear plates, and light-load sliding components. Nylon is preferred when higher mechanical strength, load-bearing capacity, and elevated temperature resistance are needed.
How to prevent warping and deformation when CNC machining nylon components?
Parts’ suppliers usually utilize pre-dried raw stock, perform stress-relief annealing prior to heavy cutting, and use razor-sharp carbide tools to minimize heat generation. On the product design side, you can maintain uniform wall thicknesses and specify balanced material removal on symmetrical faces to preserve internal stress equilibrium.
Why is stress-relief annealing critical for heavy-section nylon machining?
Extruded nylon stock retains internal stresses from manufacturing that release unevenly during material removal, causing thin walls or long plates to bow. Heating the stock to a controlled temperature (typically around 140°C–150°C) followed by gradual cooling relieves these residual stresses before final precision pass cuts.
The technical information and manufacturing advice shared on the VMT website are for general guidance only. While we strive for accuracy, VMT does not guarantee that the processes, tolerances, or material properties mentioned are applicable to every specific project. Any reliance you place on such information is strictly at your own risk. It is the buyer's responsibility to provide definitive engineering specifications for any production orders. Final specifications and service terms shall be subject to the formal contract or quotation confirmed by both parties.


 +86 15099911516



 Read more