16 years one-stop China custom CNC machining parts factory
Hey there I’m VMT Sam!
With 25 years of CNC machining experience we are committed to helping clients overcome 10000 complex part-processing challenges all to contribute to a better life through intelligent manufacturing. Contact us now
 467 |
Published by VMT at Oct 14 2026 | Reading Time:About 8 minutes


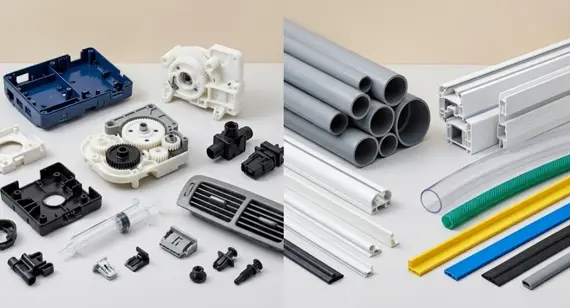
When selecting a plastic fabrication method, Injection Molding and Extrusion Molding are two of popular yet different processes. Understanding their capabilities, material compatibility, tooling investment, and part complexity is vital to avoiding costly production mistakes.
This article provides a clear, data-driven comparison between injection molding and extrusion molding. You’ll learn how both processes compare in terms of surface finish, durability, part complexity, and production cost. Furthermore, this bolg aims to address common production pain points, such as cross-sectional variations in extrusion and high upfront tooling expenses, and explore how secondary processes like precision CNC machining ensure your parts meet strict design specifications.
Additionally, we will share how we helped a medical device industry client conduct CNC machining trial production validation for PEEK rehabilitation medical device components, and subsequently evaluated following injection molding mass production processes to achieve high-efficiency(ahead of 5 weeks), low-risk mass production.
In the custom manufacturing industry, injection molding and extrusion molding are two of the most widely used plastic shaping techniques. While both share the goal of transforming raw plastic polymers into finished or semi-finished parts, they operate through fundamentally different mechanisms and suit different applications.
Before diving into the detailed breakdown, here is a quick data-driven comparison table highlighting the core differences:
| Comparison | Injection Molding | Extrusion Molding |
| Process Type | Discontinuous, closed-mold batch process | Continuous, open-die profile process |
| Part Complexity | High (Complex 3D shapes, undercuts, ribs, bosses) | Low to Moderate (Uniform, continuous 2D cross-sections) |
| Typical Tolerance / Precision | High (± 0.05 mm to ± 0.1 mm) | Moderate to Low (± 0.1 mm to ± 0.5 mm) |
| Surface Finish (Ra) | Excellent (Ra 0.4- 1.6 μm) depending on mold finish | Good to Moderate (Ra 1.6 - 3.2 μm) |
| Surface Texture | Highly customizable (matte, leather grain, geometric via mold texturing) | Limited to smooth or linear textured surfaces defined by the die |
| Product Durability | High structural integrity, uniform density, ideal for load-bearing parts | Excellent longitudinal strength, but vulnerable to transverse stress |
| Initial Tooling Cost | High (Complex multi-cavity steel/aluminum molds) | Low to Moderate (Simpler metal extrusion dies) |
| Unit Production Cost | Very low for high-volume mass production | Very low for long, continuous production runs |
Note: Since this article compares the application, cost, selection, part precision, and surface quality details of part production between injection molding and extrusion molding, and while extrusion molding can produce both plastic and metal extrusions(e.g. aluminum), injection molding is primarily a plastic mass-production process; therefore, all part comparisons in this article are conducted within the dimension of plastic part manufacturing.
1. Part Complexity (Replacing Tooling)
2. Surface Finish & Surface Texture
3. Product Durability & Mechanical Strength
4. Cost Structure (Tooling vs. Unit Cost)
5. Compatible Plastics & Melt Behavior
6. End-Use Applications
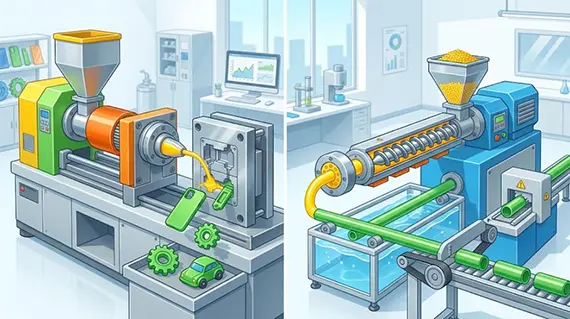
Injection molding is a premier mass-production process known for its ability to produce complex, highly repeatable 3D plastic components. To meet demanding engineering specs, injection-molded blanks often undergo secondary operations, such as CNC precision machining, for critical features like tight-tolerance holes, threads, or specialized mating surfaces.
The standard cycle follows six core steps: clamping, injection, packing, cooling, mold opening, and part removal. While highly efficient, understanding its trade-offs is essential before committing to tooling.
Key Advantages
Critical Considerations ( Limitations )
Substantial Initial Tooling Investment:Precision steel or aluminum molds require significant upfront capital expenditure.
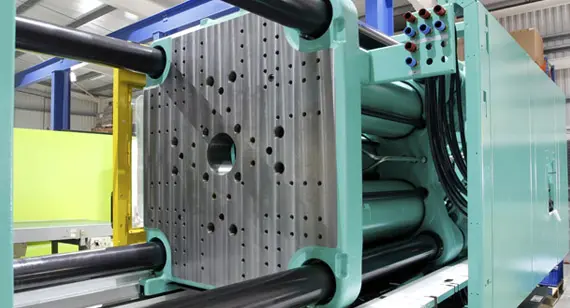
Plastic extrusion molding is a continuous, high-throughput manufacturing process designed to convert raw thermoplastic materials into profiles with uniform cross-sections. The process involves feeding polymer pellets into a heated barrel, melting and homogenizing the resin via a rotating screw, and continuously forcing the extrudate through a specialized die before cooling and sizing it in a water bath or air rack. In custom manufacturing, extruded profiles (such as thick-walled tubes, rods, or custom profiles) often serve as high-quality blank stock for secondary precision CNC machining, allowing you to add complex features like mounting holes, precision threads, or cross-cuts.
In fact, many high-volume production projects requiring extruded parts, whether the plastic components discussed in this article or extruded metal profiles like aluminum extrusions, often involve CNC machining suppliers partnering with extrusion factories to produce near-net-shape blanks. These blanks are then further refined using CNC machining to execute precision geometries, significantly saving raw material costs and accelerating production lead times.
Key Advantages
Critical Considerations ( Limitations)
Dimensional deviation and cross-sectional warping are common challenges in plastic extrusion, typically caused by uneven cooling rates, material shrinkage, or thermal stress as the polymer exits the die. To guarantee strict tolerances, professional manufacturing factories solve these issues through a combination of advanced process control and secondary operations:
Injection molding requires a substantial upfront investment for complex metal molds, but offers extremely low per-unit costs at high volumes. Extrusion molding features much lower initial tooling expenses and is exceptionally budget-friendly for continuous linear production.
When to Choose Which:
What to Do If Total Production Costs Exceed Expectations?
What If Extruded Parts Lack Sufficient Durability?
If extruded components experience frequent cracking, low impact resistance, or structural weakness under transverse stress during real-world use, you can address these durability issues through the following process optimizations or alternatives:
1. The Role of Precision CNC Machining
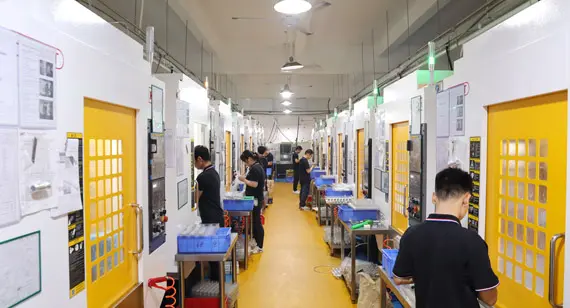
While injection and extrusion molding excel at mass-producing base shapes, achieving extreme precision on functional features can be challenging due to material shrinkage, cooling draft angles, or mold parting lines.
CNC machining steps in post-molding to refine critical areas that demand micro-tolerances:
2. Other Integration Across the Production
Beyond post-machining, other hybrid manufacturing approaches bridge the gap between design and full-scale production:
High-Precision PEEK Rehabilitation Medical Components, From CNC Prototyping to Injection Molding Scale-Up
A leading European medical device company was developing a next-generation motorized knee rehabilitation joint requiring structural housings made from biocompatible PEEK (Polyetheretherketone). PEEK was selected for its exceptional mechanical strength, wear resistance, and ability to withstand repeated chemical sterilization. However, the component featured tight functional tolerances (±0.02 mm on bearing bores) and complex internal mounting features. Facing an estimated $45,000 upfront injection mold investment and an 8-week tooling lead time, the client needed a low-risk strategy to validate the mechanical design, fitment, and thermal stability under real clinical load conditions before committing to expensive hard tooling.
Solutions: Trial Production & Validation
To mitigate financial and technical risks, our engineering team suggested that the client select CNC machining for low-volume trial production directly from extruded PEEK rod stock. Within 6 business days, our engineering team delivered 30 fully functional PEEK prototype sets. During dynamic stress testing, the CNC-machined trial parts allowed the client’s R&D team to identify a minor structural weakness near the pivot pin and optimize the wall thickness from 2.5 mm to 3.2 mm. By resolving these critical design flaws at the CNC prototyping stage, the client avoided a potential $12,000 mold modification fee and weeks of tooling rework delays.
Once the final component geometry was verified through CNC testing, our turn-key partner injection molding factory performed comprehensive Design for Manufacturability (DFM) and Moldflow simulations to transition the design to high-volume injection molding. Because PEEK requires high processing temperatures (melting point around 343°C and mold temperatures above 160°C), the injection molding factory engineered a specialized single-cavity hardened steel mold with integrated oil heating channels to prevent shrinkage deformation. To ensure the ultra-tight ±0.02 mm bearing bore tolerance was consistently maintained across mass production, we implemented a hybrid manufacturing approach: our partner injection molding factory produced the complex molded blanks, which were then delivered to our facility for secondary CNC precision reaming on the critical internal bore.
Final Results: High-Efficiency, Low-Risk Mass Production
This staged hybrid manufacturing strategy delivered outstanding commercial and technical outcomes for the client. Transitioning from full CNC machining to injection molding reduced the per-unit production cost by 68% (from $125/unit down to $40/unit) at a monthly volume of 5,000 units. Cycle times dropped dramatically from 28 minutes per CNC machined part to just 45 seconds per molded part, while maintaining a 99.4% first-pass yield rate. By combining rapid CNC machining for design validation with optimized injection molding for mass production, our turn-key service team enabled the client to launch their rehabilitation device to market 5 weeks ahead of schedule with zero tooling write-off risk.
At VMT, we go beyond traditional single-process manufacturing. As a premier precision facility, we integrate high-precision CNC machining, custom injection molding, and plastic extrusion services under one roof. Whether you need rapid prototypes to validate your design, bridge production to beat strict deadlines, or high-volume mass production, VMT delivers high-quality, ultra-precise plastic components tailored to your exact specifications.
By seamlessly bridging CNC precision machining with injection and extrusion molding, we solve your toughest manufacturing challenges—from initial sampling to secondary post-machining on critical features—ensuring exceptional quality, cost efficiency, and fast turnaround.
Choosing VMT as your manufacturing partner, you will get:
At VMT, we are committed to being your reliable manufacturing collaborator, helping you reduce engineering risks, optimize production budgets, and bring superior plastic products to market faster.
Both injection molding and plastic extrusion molding play vital, distinct roles in modern plastic manufacturing. Choosing the optimal route depends on your part geometry, required tolerances, surface finish, production volume, and budget constraints.
When standard molding alone cannot meet tight tolerance demands, integrating secondary CNC machining provides the perfect hybrid solution. Whether you require continuous profiles, intricate 3D molded parts, or high-precision post-machined components, we offers the expertise and end-to-end manufacturing services needed to bring your project to life with confidence. Contact us with your drawings for free tailored manufacturing solutions! [2D Drawings (PDF files), 3D Drawings (IGS/STP/STEP files)].
Send your drawings, requirements, and target quantity. VMT will review your project and provide a machining solution and quote.
All information and uploaded files are secure and confidential.
1 Tell us what you need
2 Get solution & quote
3 Approve production
Email: inquiry@vimetal.com.cn
1. Which has a longer lead time: injection molding or plastic extrusion molding?
Injection molding typically has a longer initial lead time. Manufacturing complex multi-cavity injection molds usually takes 4 to 8 weeks, whereas extrusion dies are simpler and can often be completed in 2 to 4 weeks. However, once tooling is validated, both processes offer extremely rapid production speeds.
2. The lead time is too long, how can I speed up production?
3. How many types of injection molding processes exist, and what are their key differences?
4. What similarities exist between extrusion molding and injection molding?
Both processes rely on thermal energy to melt thermoplastic pellets, use rotating screws within heated barrels to homogenize the polymer melt, and require downstream cooling mechanisms to finalize the geometry. Furthermore, both can utilize secondary CNC machining to add precision threads, tight-tolerance holes, or custom cutouts.
5. Is plastic extrusion molding primarily used in the construction industry?
While construction is a major market (for pipes, window frames, and conduit), plastic extrusion is equally vital in medical (catheter tubing, fluid lines), automotive (weather stripping, wire jacketing), and consumer packaging (films, food-grade tubing) industries.
6. CNC Machining vs. Injection Molding: What are the main differences?
CNC Machining vs. Injection Molding: CNC machining is a subtractive process that cuts parts out of solid plastic stock without upfront tooling; injection molding is a formative process that injects liquid resin into a custom mold. Additionally, CNC machining is ideal for low-to medium-volume production and rapid design iterations, while injection molding is cost-effective for high-volume mass production .
The technical information and manufacturing advice shared on the VMT website are for general guidance only. While we strive for accuracy, VMT does not guarantee that the processes, tolerances, or material properties mentioned are applicable to every specific project. Any reliance you place on such information is strictly at your own risk. It is the buyer's responsibility to provide definitive engineering specifications for any production orders. Final specifications and service terms shall be subject to the formal contract or quotation confirmed by both parties.


 +86 15099911516



 Read more