16 years one-stop China custom CNC machining parts factory
Hey there I’m VMT Sam!
With 25 years of CNC machining experience we are committed to helping clients overcome 10000 complex part-processing challenges all to contribute to a better life through intelligent manufacturing. Contact us now
 421 |
Published by VMT at Sep 28 2026 | Reading Time:About 6 minutes


Can you distinguish between chemical etching, laser etching, laser engraving, and laser marking, and make the right engineering choice among them for CNC machined products? Understanding their process characteristics, pros and cons, practical results, and costs will help you make informed decisions and tackle project challenges.
For instance, serial numbers or QR codes wearing off over time can lead to inspection failures or traceability issues. Improper marking methods on thin-walled precision parts can cause slight deformations, exceeding tolerances and increasing scrap rates. Or perhaps you want to achieve an Apple-style textured surface on aluminum parts using an etching process, but the final appearance fails to meet your expectations. This article aims to help you clearly understand their core characteristics and make the right choice across various application scenarios.
At the end of this article, we will also share a case study on how our facility used etching to deliver a silky, anti-glare, fine-touch surface finish similar to Apple products, paired with laser etching to produce crisp, permanent labels that never fade.

Only use one sentence to let you understand thier relationships: "Etching" usuallly refers to chemical etching ( or plasma etching), while "Laser Etching"( not the etching category) and "Laser Engraving" are specialized sub-branches of Laser Marking.
Choosing the wrong process not only wastes budget but also directly affects part precision and aesthetic quality. The table below compares the key characteristics of Chemical Etching, Laser Etching, and Laser Engraving to help you make a quick decision.
| Process Name | Mechanism | Surface Micro-Morphology | Typical Depth | Cost |
| Chemical Etching (what we often say “Etching” ) | Chemical / Plasma Dissolution (Acid, alkali, or plasma selectively dissolves exposed material) |
Recessed / Through-hole (Smooth edges, zero Heat-Affected Zone, stress-free) |
Adjustable (From 0.0005" up to full cut-through) |
High setup cost (photomasks), Low per-unit cost for high-volume batch processing |
| Laser Etching (Laser Marking Branch) | Localized Melting and Expansion (Laser beam melts the surface; material expands and resolidifies) |
Micro-Convex / Raised Bumps (Slightly raised micro-texture with minimal indentation) |
Very Shallow (Typically ~0.001") |
Low operational cost, highly cost-effective for mass production lines |
| Laser Engraving (Laser Marking Branch) | High-Energy Vaporization / Ablation (Laser beam vaporizes material to carve out physical depth) |
Recessed Cavity (Clear tactile depth, distinct sharp-edged grooves) |
Deep (0.010" to 0.020"+ depending on material and passes) |
Medium to High (Requires higher laser power and longer cycle times per part) |
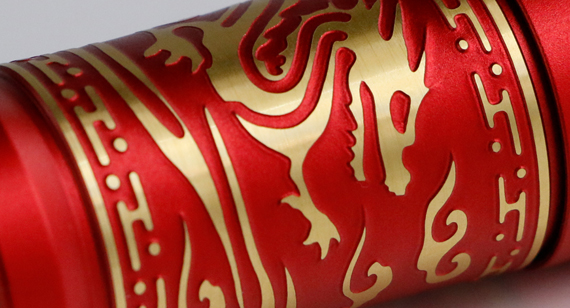
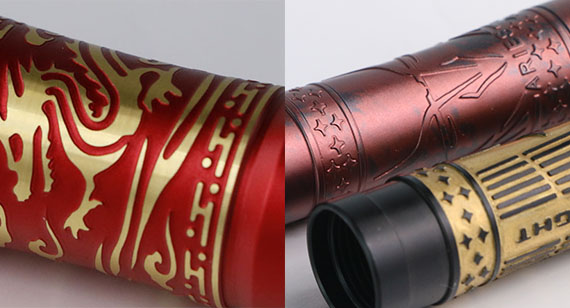
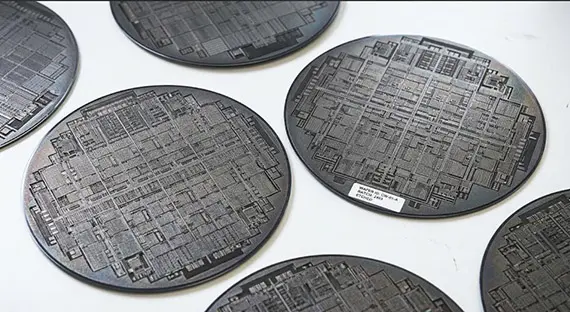
Etching (including Wet Chemical Etching and Dry Plasma Etching) is a manufacturing technique that uses chemical or acidic solutions to create recessed patterns or text on metal and non-metal surfaces. Traditionally, artists and hobbyists have used this process to craft highly detailed and expressive printmaking artwork. In modern manufacturing, it is widely utilized to produce crisp patterns and fine lines on electronics enclosures, semiconductors, medical components, and custom automotive CNC machined parts, delivering exceptional corrosion resistance without introducing thermal stress.
Here is a look at the typical process flow:
1. Material Selection and Preparation: Suitable materials commonly include copper, stainless steel, titanium, zinc alloys, steel, silicon wafers, and ultra-thin metal foils (<0.1 mm). The surface of the CNC machined part intended for etching is thoroughly polished and cleaned.
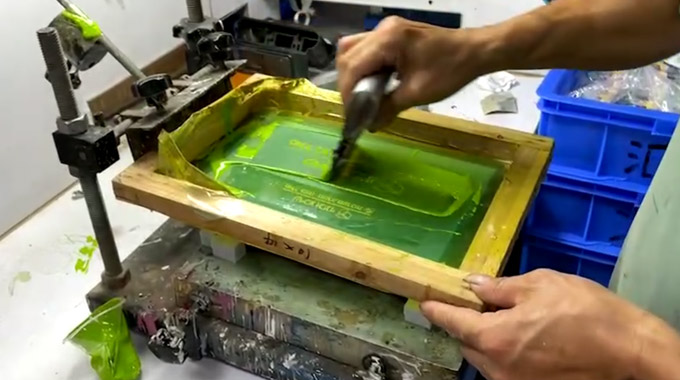
2. Applying the Protective Layer (Masking): An acid-resistant mask is applied to the part surface to block direct contact with the chemical solution.
3. Pattern Inscription (Scribing or Developing):
In traditional art/craft applications, a sharp scribing tool is used to scratch through the wax layer to expose the underlying metal. In modern industrial photolithography, the exposed photoresist is developed away, smoothly revealing the precise areas intended for etching without any manual scratching.
4. Acid Bath / Etching: The part is immersed in an acidic bath (or exposed to reactive plasma). The chemical solution dissolves the exposed material where the protective mask was removed, creating smooth-edged, recessed features or burr-free through-holes.
5. Mask Removal: Finally, the remaining protective wax, varnish, or photoresist layer is chemically stripped away to reveal the finished part.
AND, below is a showcase of semiconductor wafers with chemical etching:
Pro and Cons of Etching CNC Machined Parts
Chemical etching offers unique engineering advantages for CNC parts, though it also comes with specific production limitations. Understanding these practical pros and cons will help you determine if this surface process fits your project requirements.
Advantages:
Limitations:
Strictly speaking, no. Calling laser etching simply "etching" is misleading in precision manufacturing and custom CNC engineering. What we say -- etching, specifically chemical or plasma etching, relies on chemical dissolution to remove material, leaving smooth recessed cavities or through-holes without heat. Laser etching, on the other hand, is a thermal process that uses focused laser energy to melt the material's surface locally, causing it to expand and re-solidify into micro-convex (raised) marks rather than dissolving material away.
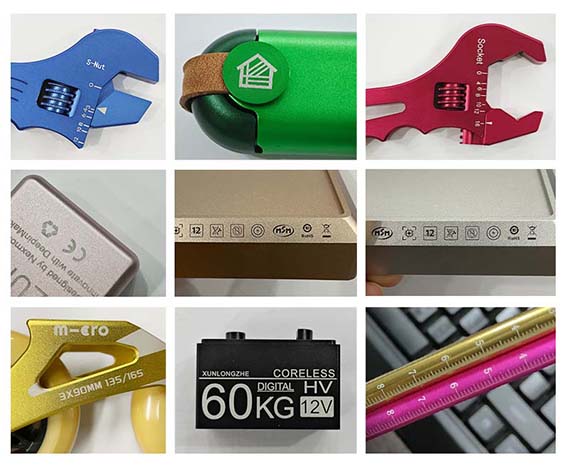
In fact, laser etching is much closer in mechanism and execution to laser engraving than to chemical etching. Both laser processes belong to the laser marking family and utilize thermal energy to modify a part's surface. The primary difference between the two lies in the physical outcome: laser engraving acts like a high-energy chisel that vaporizes material to cut deep, concave grooves into the surface, whereas laser etching merely melts and swells the top layer to create a high-contrast, slightly raised tactile texture.
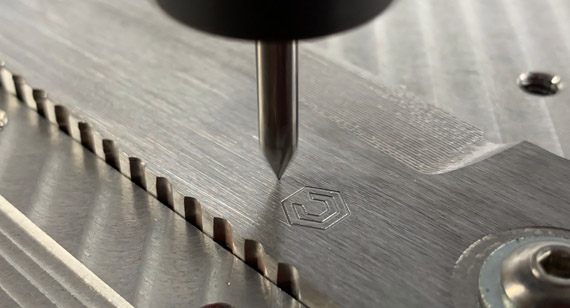
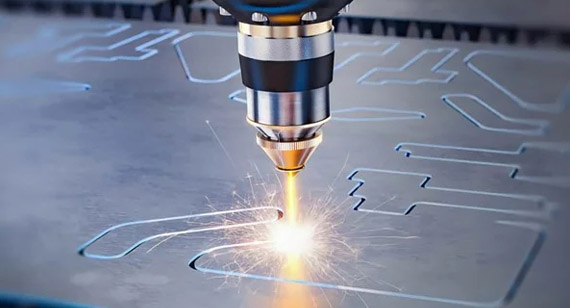
Laser engraving is a precise thermal ablation process that uses a high-energy laser beam to vaporize material from a substrate's surface, carving out clean, deep recessed cavities. Unlike chemical etching or shallow laser etching, laser engraving creates high-contrast, permanent markings with exceptional wear resistance. It operates as a non-contact, force-free method suitable for a wide range of metals and non-metals in precision CNC manufacturing.
You can use it across industries such as electronic communications, automotive manufacturing, medical devices, and precision hardware to produce high-precision serial numbers, brand logos, QR codes, and wear-resistant warning labels.
Process:
Pros and Cons of Laser Engraving CNC machined Parts
Laser engraving has excellent wear resistance, deep tactile contrast, permanent physical grooves, while it also has slower processing speed and creates slight thermal impact and debris at the edges.
Advantages:
Disadvantages:
Depth and Tactile Texture
When choosing between chemical etching and laser engraving, depth and tactile feel are primary considerations.
When the application demands an ultra-smooth finish or micro-fluidic channels, chemical etching is the superior choice. However, if clear, tactile markings with visible depth are required, laser engraving is far more suitable.
Material Stress and Heat-Affected Zone (HAZ)
Material stress and the Heat-Affected Zone (HAZ) directly impact the geometric precision and structural integrity of critical components.
Therefore, chemical etching is recommended for tight-tolerance, stress-intolerant precision components.
Durability and Wear Resistance
Durability dictates marking longevity under high-friction use conditions.
For heavy machinery, tooling, or components subject to relentless friction and physical wear, laser engraving provides a much higher margin of durability safety.
Manufacturing Efficiency and Volume Costs
The trade-off in processing efficiency depends heavily on production scale and sheet-level.
Consequently, chemical etching holds a decisive cost advantage for volume sheet-metal fabrication, whereas laser engraving is far more economical for short or medium runs.
Part Traceability and Industry Compliance
Traceability and regulatory compliance are essential mandates in modern manufacturing.
For the primary objective: part serialization, laser engraving is the compliant, industry-standard choice.
This article provides an in-depth engineering comparison between chemical etching and laser engraving for custom CNC components, evaluating their processing mechanisms, dimensional tolerances, tactile depths, and volume cost structures. To clarify common industry terminology confusion, we've also metioned the laser marking, and laser etching. Overall, you can choose etching for stress-free batch processing, micro-channel features, and achieving silky, anti-glare satin finishes without introducing thermal stress or altering tight tolerances. Conversely, Laser Engraving is essential when physical ablation and maximum resistance to severe friction are non-negotiable, while Laser Etching provides a rapid, cost-effective method for post-anodization serialization and high-contrast labeling. Struggling to choose between chemical etching and laser processes for your complex CNC components? Contact us and let our engineering team recommend the optimal surface finishing strategy to ensure your parts meet Ra roughness, tolerance, marking and durability specs. [2D Drawings (PDF files), 3D Drawings (IGS/STP/STEP files)].
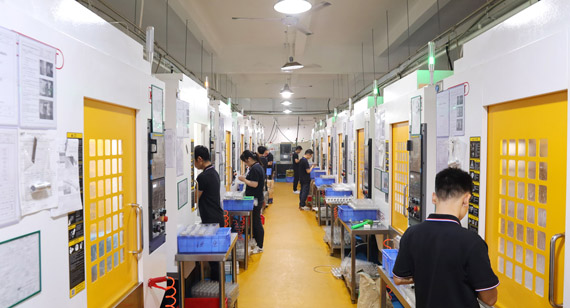
Combining Chemical Bath Flattening And Low-Depth Fiber Laser Etching For Precision Medical Devices To Achieve a Silky, Anti-Glare, Fine-Touch Surface Finish And High-Contrast Markings.
A medical client engaged our team to manufacture custom aluminum enclosures for handheld diagnostic devices. The project required an ultra-smooth, anti-glare finish capable of withstanding strict clinical sanitization routines, alongside high-contrast branding and regulatory markings that would remain clear across years of intensive daily handling.
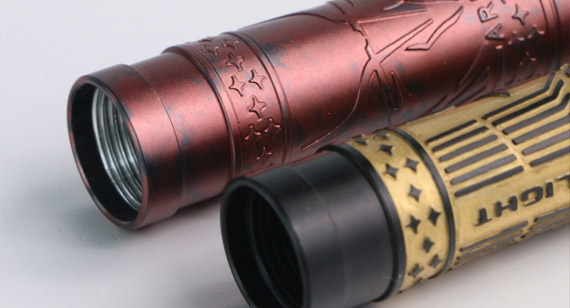
To achieve the specified tactile quality and optical performance, we implemented a controlled chemical etching process prior to anodization. The raw 6061-T6 aluminum shells were subjected to a chemical bath that uniformly dissolved 3 µm to 5 µm of material across all exposed surfaces. This uniform material removal flattened surface peaks, reducing the surface roughness from an initial Ra 1.6 µm down to a consistent Ra 0.4 µm–0.8 µm range while removing directional CNC machining lines to deliver a silky, anti-glare, fine-touch surface finish.
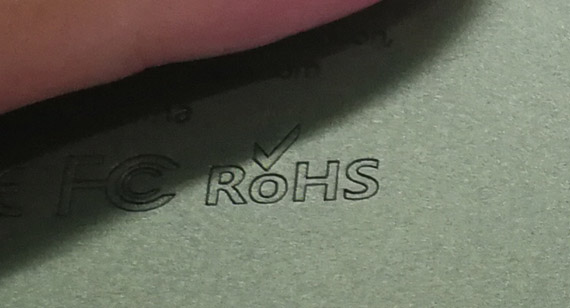
Following chemical treatment and clear anodization, the parts were transferred to our laser marking cell for secondary processing. Using a high-precision fiber laser system calibrated to low-pulse thermal etching parameters, we modified only the top anodized layer without penetrating the underlying aluminum substrate. Because this thermal reaction operates strictly within a depth of less than 25 µm, the process added zero dimensional variation, fully preserving the strict ±0.02 mm overall tolerances.
The integrated process delivered a surface finish that passed full CMM dimensional inspection and strict cosmetic grading. Inspection confirmed zero boundary deviation on critical mating surfaces, complete absence of optical glare under intense operating room lighting, and 100% legibility of the high-contrast laser markings after 500+ cycles of IPA and hospital-grade disinfectant wipe-downs.
Send your 2D drawings, 3D CAD models, material, marking or etching requirements, target depth, surface finish, tolerance, quantity and application. VMT will review the suitable process, DFM, finishing route and quotation requirements.
All information and uploaded files are secure and confidential.
1 Tell us what you need
2 Get solution & quote
3 Approve production
Email: inquiry@vimetal.com.cn
1. Is laser etching less wear-resistant than chemical etching and laser engraving?
Yes, laser etching is generally less wear-resistant compared to both deep laser engraving and chemical etching. Because laser etching only melts and expands the very top layer of the material (typically reaching a shallow depth of around 0.001 inches), the resulting micro-convex surface marks can wear down over time under continuous heavy friction or harsh mechanical abrasion.
In contrast:
2. Should I avoid laser etching due to its lower durability?
Not necessarily. While laser engraving or chemical etching is recommended for CNC machined components subject to severe friction and harsh abrasive conditions, laser etching remains an excellent choice for many applications due to its unique benefits:
3. Can laser engraving and chemical etching be performed on non-metallic CNC materials like plastics or ceramics?
Yes. Laser engraving easily processes engineered plastics, high-density polymers, and technical ceramics via direct thermal ablation, whereas chemical etching for non-metals requires specialized chemical reagents (such as hydrofluoric acid for glass or specialized etchants for ceramics) rather than standard metal acids.
4. How does chemical etching affect the corrosion resistance of stainless steel components?
Chemical etching exposes fresh bare metal, which temporarily removes the native passive oxide layer. However, following a standard post-etch passivation treatment (such as a citric or nitric acid bath), full corrosion resistance is completely restored across all etched surfaces.
5. Is it possible to control the color contrast of laser-engraved markings on un-anodized raw metals?
Color contrast on raw metal is limited because laser engraving physically carves out bare material, usually resulting in a matte, monochromatic surface finish. Achieving bright white or dark black contrasting marks without deep physical depth is typically accomplished using lower-power laser etching or laser dark-marking parameters rather than deep ablation engraving.
6. Does chemical etching create dangerous undercutting beneath the photoresist mask?
Chemical etching is inherently isotropic, meaning it dissolves metal laterally beneath the edges of the phototooling mask at roughly the same rate it etches downward. Engineers account for this known factorduring early CAD/phototooling design by adjusting mask boundaries, ensuring the final feature geometry meets exact technical drawing dimensions.
The technical information and manufacturing advice shared on the VMT website are for general guidance only. While we strive for accuracy, VMT does not guarantee that the processes, tolerances, or material properties mentioned are applicable to every specific project. Any reliance you place on such information is strictly at your own risk. It is the buyer's responsibility to provide definitive engineering specifications for any production orders. Final specifications and service terms shall be subject to the formal contract or quotation confirmed by both parties.


 +86 15099911516



 Read more