16 years one-stop China custom CNC machining parts factory
The VMT blog is dedicated to sharing our hard-earned knowledge in prototype manufacturing. We hope these articles will help you optimize your product designs and gain deeper insight into the world of rapid prototyping. Enjoy the read!
Get an Instant Quote All uploads files are safe and confidential
 VMT
 2026 11 07
While commodity aluminum prices (LME) typically fluctuate between $2.30 and $2.70/kg( last ten years, but now in 2026 it’s been $2.90 ~ $3.40 /kg affected by the energy), raw material costs are only one part of the final CNC machining quote. In general, aluminum material procurement accounts for approximately 20%–45% of the total quoted price, while the remaining 55%–80% comes primarily from CNC machining time, tooling and fixtures, workholding and setup, and surface finishing.
 66
 Read more
 VMT 2026 11 07
Not all stainless steel is magnetic. Its magnetic properties mainly depend on its metallurgical structure, specific grade, and processing condition. In general, austenitic stainless steels (such as 304, 316, and 316L) are typically non-magnetic or weakly magnetic in the annealed condition, while ferritic stainless steel (such as 430) and martensitic stainless steels (such as 410, 420, and 440C) are generally magnetic. In addition, austenitic stainless steels such as 304 may develop some magnetism after cold working, bending, or significant mechanical deformation due to strain-induced martensite formation. For CNC precision stainless steel parts, magnetism is relevant to material selection, machining processes, and final application requirements. For example, MRI equipment, precision sensors, and other devices sensitive to magnetic fields require particular attention to the material's relative magnetic permeability.
66
Read more
 VMT 2026 11 04
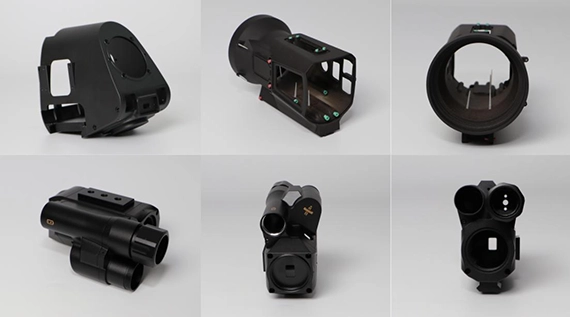
For custom CNC machining projects involving night vision and thermal imaging equipment housings, tolerance design, sealing design, and cost optimization require careful consideration during the design stage. This includes defining the primary optical datum, optimizing internal corner radii, allowing 0.02–0.05 mm for coating thickness compensation, and selecting suitable materials based on the actual operating environment. For example, 7075-T6 aluminum is suitable for high-strength, lightweight UAV imaging housings, while corrosion-resistant 316L stainless steel is a suitable choice for marine monitoring imaging housings. These considerations help reduce CNC machining costs and scrap and rework costs while meeting requirements for boresight shift below 0.5 MOA and IP67/IP68 protection.
66
Read more
 VMT 2026 11 04
Precision manufacturing of robotic joint housings should not focus solely on the dimensional accuracy of individual components. It also requires establishing a unified datum system centered on the main rotational axis from the design stage, as well as evaluating the manufacturer's machining experience and capabilities. For example, manufacturers should adopt one-setup multi-axis machining whenever possible to minimize cumulative errors caused by repeated repositioning. Only by aligning design datums, machining accuracy, and assembly requirements can alignment deviations and assembly rework risks be effectively reduced.
66
Read more
 VMT 2026 11 03
When developing custom CNC motorcycle brake and clutch levers, the key is not simply to achieve the desired appearance or lightweight structure. It is equally important to ensure accurate geometric relationships and reliable assembly fits in critical functional areas, such as pivot holes, bearing seats, and actuation contact surfaces, while considering material properties, surface finishing, and manufacturability for batch production.
66
Read more
 VMT 2026 10 30
Successful custom CNC EDC parts production depends on more than achieving tight machining tolerances. Material selection, wall thickness, thread and moving clearances, surface-treatment allowances, cosmetic requirements, and inspection methods must be planned together from the design stage. When these factors are controlled through DFM, precision CNC machining, and prototype validation, manufacturers can achieve smoother assembly, more consistent finishes, lower scrap rates, and a reliable transition from prototypes to mass production.
66
Read more
 VMT 2026 10 28
In aerospace, defense, and energy applications, components must operate reliably under extreme temperature, pressure, and corrosive environments. Many stainless steels, and even common titanium alloys, lose structural strength rapidly at temperatures exceeding 600°C. To meet these harsh demands, Waspaloy CNC machining has become a critical manufacturing solution for high-reliability components.
66
Read more
 VMT 2026 10 28
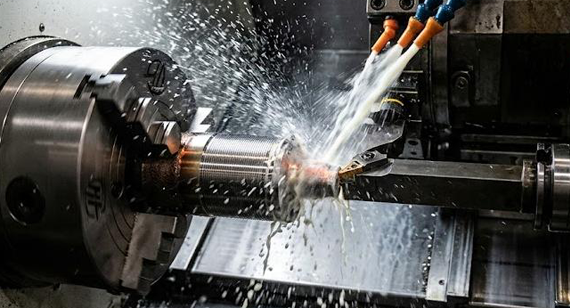
As a nickel-molybdenum-chromium superalloy engineered for high-pressure and corrosive environments, Hastelloy maintains structural stability at temperatures above 540°C, making it widely specified in aerospace and demanding chemical processing sectors. However, producing complex hastelloy components introduces distinct manufacturing risks. Without controlled feed rates, targeted coolant delivery, and rigid fixturing, processing frequently leads to rapid tool degradation, thread galling, and geometric distortion in thin-walled features. Through 5-axis toolpath optimization and phased finishing sequences, complex Hastelloy structural components can achieve a 99.2% first-pass yield rate and tight tolerances of ±0.008 mm (demonstrated in the case study section below).
66
Read more


 +86 15099911516